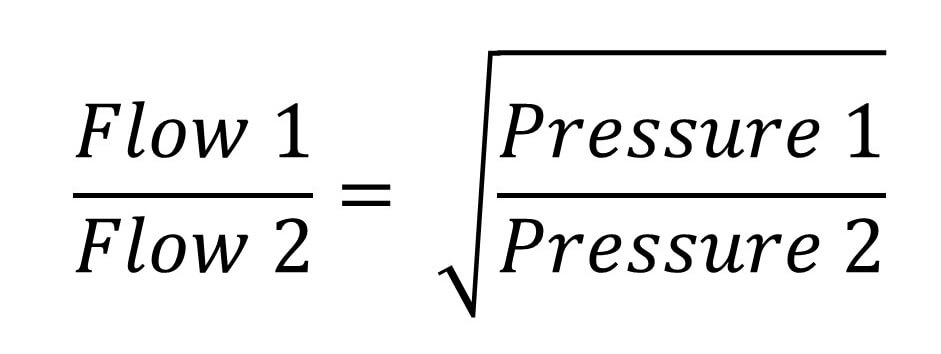Category: Boom Sprayers

Main category for sprayers with horizontal booms

  • Storing Pesticide Mix Overnight

    Storing Pesticide Mix Overnight

    Not being able to finish a tank due to weather or any other reason happens to just about everyone. Is it OK to simply leave the sprayer as is, and resume spraying later after some agitation?

    In many cases, the answer is yes. Most pesticide mixtures are stable in short term storage. On resuming spraying, an agitation could be all that’s needed to get back to where you started a day or so earlier.

    But there are three important exceptions.

    When the active ingredient is formulated as a suspension. Suspensions are typically wettable powders and flowables, and rely on a clay carrier to distribute the active in the tank. Because clay is denser than water, these formulations settle out quickly after agitation stops. Sure, they can be brought back into suspension with vigorous agitation. But in lines and booms, boom ends and screens, dislodging a settled clay carrier is much more difficult. It’s also hard to tell if the cleaning has been successful because the problem spots are hidden.

    The best solution is to flush the spray boom with water before materials can settle and lodge. A visual inspection where access is possible, such as strainer bowls and boom ends, is part of the process to ensure the formulated product has been removed.

    Learn to identify which formulations are suspensions. There’s lots of jargon out there. Look for terms such as DC, DF, DG, DS, F, Gr, SP. Even EC formulations are suspensions (oil in water) and require agitation.

    When the active ingredient is chemically unstable. Some pesticides can degrade in the tank, usually due to alkaline (high pH) hydrolysis. The effect is very pesticide specific, but in general, insecticides (particularly organophosphates and carbamates) are more susceptible than other pesticides. This fact sheet by Michigan State University describes the impact of pH on a the half-life of a large number of pesticides.

    Note that in the examples in the MSU fact sheets, pesticide half lives are typically days and weeks, and only rarely hours. Also note that while high pH is most often problematic, low pH can lead to faster breakdown in a small number of products.

    Ensuring tank mix stability requires a pH meter or paper, and possibly a pH modifier such as citric acid. But do your research first! Here’s an article on pH and water quality.

    When the tank previously contained a product known to harm the current crop. This situation is most common and most difficult to address. Some examples from western Canada are Group 2 modes of action sprayed prior to a canola crop. Why are Group 2 products implicated?  Many are formulated as dry products on a clay base, and these can settle in boom ends, adhere to tank walls, or get stuck on screens. Their solubility is pH dependent, as we explain in this article.

    Canola is particularly sensitive to this mode of action, and the most common canola herbicides, Liberty and glyphosate, are formulated with strong detergents that act as tank cleaners.

    Even when applicators think that their tank is clean, they can’t actually be sure and can’t do much about it at that stage. The stripping of tiny amounts of residue off the tank walls, filter screens, or plumbing, can happen during a mid-day stop or an overnight break.  Applicators eventually find out that this happened, usually about two weeks after spraying.

    Our advice is:

    After spraying a herbicide to which a subsequent crop may be sensitive, with the classic case being a Group 2 and moving to canola, be extra diligent with cleaning and pay attention to the tank walls, all screens, and boom ends.

    The best way to solve issues is to avoid them in the first place. If the weather looks unsettled and may interrupt your spray operation, consider mixing smaller batches that can be sprayed out completely even if conditions change quickly. This allows you to rinse the tank and spray water through the boom, thus avoiding a contamination problem developing overnight.

    If that’s not possible, at least do not let a tank mix sit in the boom overnight. Instead, use your clean water tank to push water through the boom prior to storage and double check the screens. The following day, prime the boom with your tank mix as usual and resume spraying the crop.

    If you’re not sure that your sprayer can draw from the clean water tank and push through the booms (the wash-down nozzles are, after all, the intended destination for that water), decipher your system and add the necessary valves that make this possible.

    A useful design that helps flush and prime a boom quickly is the recirculating boom offered by some aftermarket boom manufacturers. These booms are also more common on European sprayers. A nice feature of such designs is that the tank contents can be pumped through the entire boom assembly without actually spraying. This ensures that the boom is primed without any soil contamination. It also dilutes whatever residue there may be in the boom plumbing with the entire tank, likely reducing its concentration enough to be of little concern.

    An additional feature of recirculating booms is that many offer stainless steel tubing throughout most of their feed and return length, minimizing the black rubber hose products that often adsorb, and later release, herbicide contamination.

    Even if a wholesale boom or sprayer change is impractical, consider switching to steel boom lines and tanks tank to minimize residue carryover.

    As is often the case in the spraying business, prevention is easier and less costly than solving a big problem later. Spray mix storage is one of those examples where a small amount of extra effort at the beginning can pay big dividends later.
  • How Do Hydraulic Low-Drift Nozzles Work?

    How Do Hydraulic Low-Drift Nozzles Work?

    Low drift nozzles have become the standard way to apply pesticides from a boom sprayer. In order to use them properly, we need to understand how they are designed and how they are intended to work.

    Sprayer nozzles have three functions on a sprayer.

    1. Metering flow
    2. Atomizing liquid
    3. Distributing liquid uniformly

    Accurate metering of the flow is done through precise machining or molding of the nozzle.

    Atomization of a liquid occurs by imposing some sort of force on the liquid that causes it to break up from a stream or a sheet into droplets of the desired spray quality.

    Distribution is done by generating a pattern that, in combination with adjacent nozzles, produces similar dosages in appropriate droplet sizes and densities, along the target area.

    All three of these functions are confirmed by the nozzle manufacturer, but the properties are likely to change with wear.

    Atomization

    Atomization forces could be air-shear (used in some aircraft, airblast, or twin-fluid nozzles), centrifugal energy (used in rotary atomizers), electrical energy (used in some electrostatic sprayers), or hydraulic pressure (used in the most common nozzles, the flat fan or hollow-cone tips).

    Typically, the higher the applied energy, the greater the break-up of the spray. More air-shear resulting from faster aircraft or fan speeds, faster rotation of a cage, or more hydraulic pressure all have similar effects: they create finer sprays.

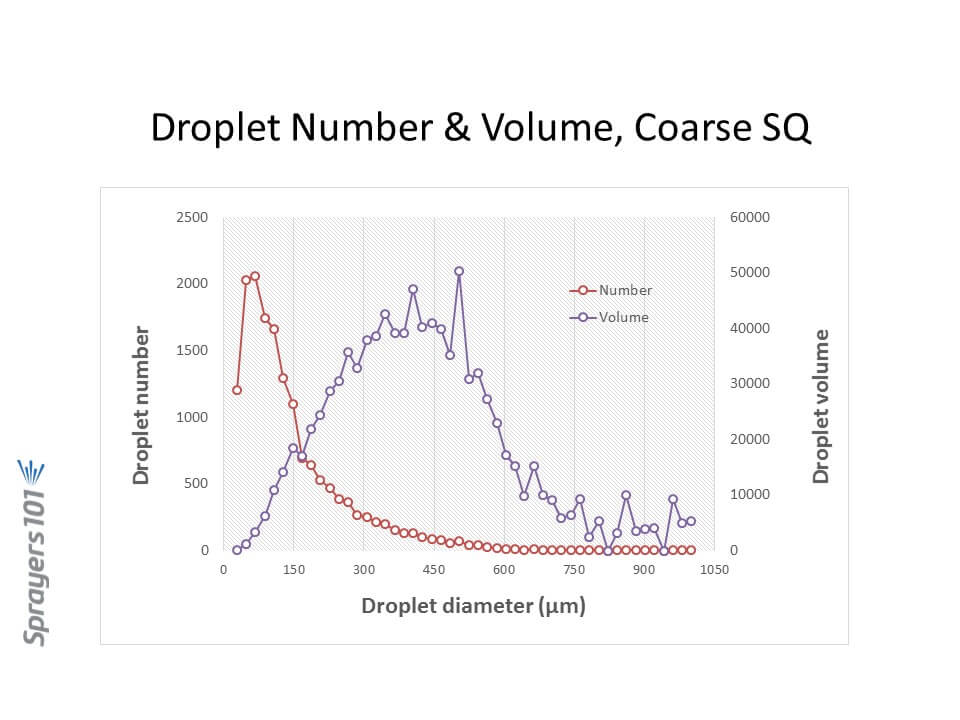
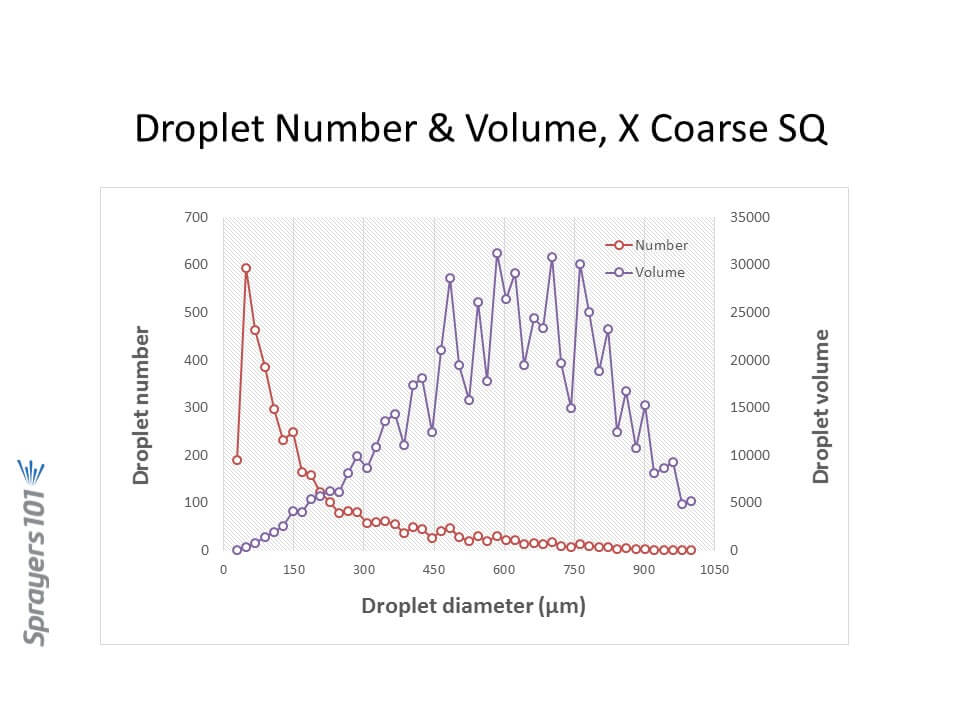
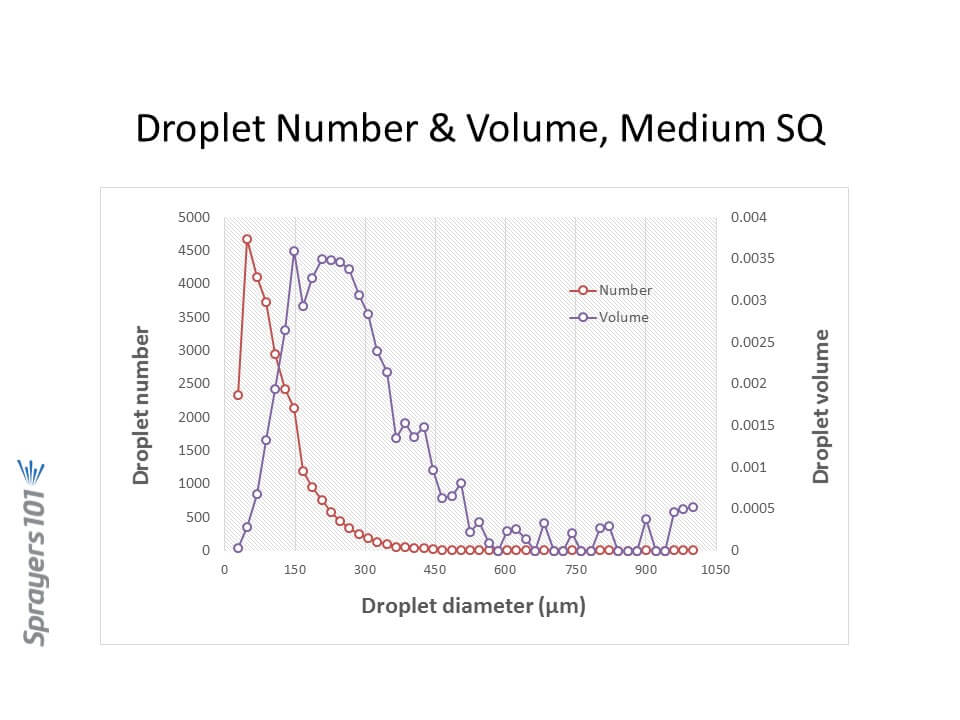
    Most nozzles produce polydisperse sprays, comprised of a large number of different droplet sizes. For hydraulic flat fan nozzles, droplets ranging from 5 to 2000 µm can be produced. The exact distribution of the volume in these droplet sizes depends on the nozzle design, the spray liquid, and the pressure. Here are three examples, representing approximately Medium, Coarse, and Extremely Coarse sprays.

    Droplet size distribution by number and volume from a Medium spray. Note the majority of the droplets are small, but the majority of the volume (dose) is in somewhat larger droplets.
    Droplet size distribution by number and volume from a Coarse spray. Like in the Medium spray, the majority of the droplets are small although there is fewer of them. The majority of the volume is in intermediate sized droplets.
    Droplet size distribution by number and volume from a Very Coarse spray. While the majority of the droplets are small as in the finer sprays, their overall number is sharply reduced from the finer sprays. The volume is now in the largest droplet sizes.

    Let’s focus on hydraulic nozzles, by far the most common in agriculture.

    Spray Pressure

    Spray pressure is a useful tool for controlling droplet size from any hydraulic nozzle. Need a finer spray?  Add pressure. It is also the basis for the age-old recommendation that lower pressures are a good tool for reducing drift.

    We impose practical limits on the upper and lower range of recommended pressures based on several other factors, chief among them the spray pattern.

    Spray patterns of a certain width, or angle, are required for proper pattern overlap. The convention is to space hydraulic nozzles at 15 or 20 inch intervals along a boom, and operate them at about 20” above the target. Boom height values will depend on the fan angle of the nozzle and the degree of overlap required. For low-drift flat fan tips, a minimum 100% overlap is best. With 100% overlap, the spray pattern width at target height is twice the nozzle spacing. With this approach, at any point under the boom, the target receives droplets from the closest two nozzle patterns.

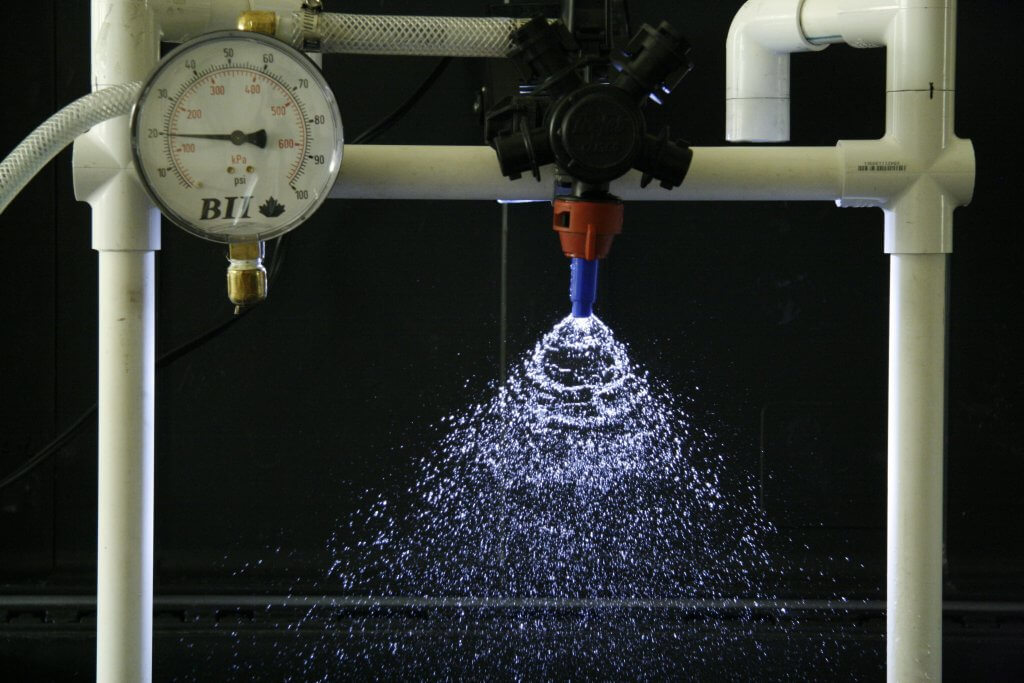
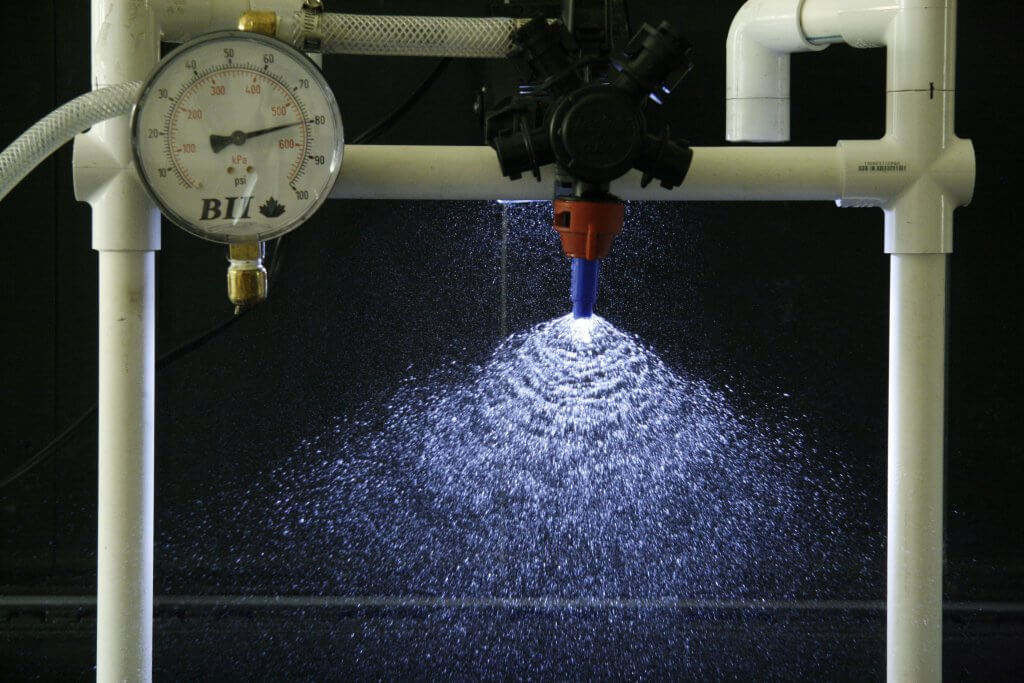
    Pattern angles are published by manufacturers, but in practice, angles often differ from those values and can vary with spray formulation. Importantly, they tend to become narrower at lower pressures. The exact pressure at which this happens depends on the tip design, but experience shows that pressures below 20 psi for conventional nozzles, and 30 to 40 psi for low-drift nozzles, result in poor (too narrow) patterns. Narrow patterns reduce overlap, resulting in poor distribution.

    TeeJet AI11003 at 20 psi
    TeeJet AI 11003 at 80 psi

    We might also limit pressures at the upper end, based on drift potential. Most conventional flat fan nozzles, for example, drift excessively at pressures above 60 psi or so, hence that limit.

    Low Drift Nozzles

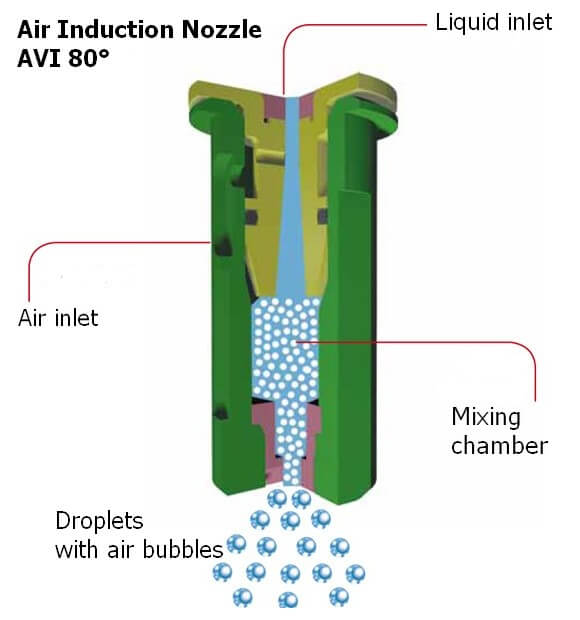
    Low drift nozzles were quickly adopted by applicators due to their ability to reduce drift and thereby widen the window of safe spray application. They work by using a two-stage design (often called “pre-orifice”) to reduce the internal operating pressure of the tip. The pre-orifice, the original liquid inlet, is round and sized for the nominal flow of the tip. The exit orifice is eliptical in shape and has a larger flow capacity than the pre-orifice, by about 1.2-fold to 2.5-fold. The larger exit creates an internal pressure drop, so the pattern formation produces larger droplets as though the operating pressure had been reduced. Most modern low-drift tips also introduce air into the nozzle via a built-in venturi. This further suppresses the formation of driftable droplets and introduces air into the interior of the nozzle, adding some pressure back to the system.. The Albuz AVI nozzle schematic below explains the venturi design.

    Cross-section of the Albuz AVI venturi nozzle.

    The tapered channel inside the nozzle is a venturi, which draws air into the nozzle via integrated ports. When low-drift nozzles are operated beside conventional nozzles at the same pressure, low-drift nozzles produce much fewer driftable fines, and also more larger droplets.

    But while the two-stage design is useful for managing drift, it also conceals the actual operating pressure of the exit orifice in these tips. The exit orifice is important – it is the part of the nozzle that does the atomizing and that forms the pattern.

    Let’s illustrate the pressure inside a low-drift tip by operating an air-induced low-drift nozzle at 60 psi. This nozzle has a pre-orifice size of 03 (0.3 US gpm at 40 psi, blue) and an exit orifice size of 06 (0.6 US gpm at 40 psi, grey). The operator sees 60 psi on the gauge. What is the exit orifice pressure?

    The exit tip has twice the flow-rate of the pre-orifice, and therefore operates at one quarter the pressure, or 15 psi. Recall the square-root relationship between flow rate and pressure.

    The relationship between spray pressure and flow rate. Doubling the flow rate requires a quadrupling of pressure

    That’s not the whole story. The internal venturi is drawing additional air into the nozzle chamber, and depending on the operating pressure, this could be from 5 to 15 psi. The amount added depends on the specific nozzle, its flow rate, and its pressure. Let’s add 10 psi in this case. The exit tip is actually at 25 psi.

    Now let’s assume the pressure gauge reads 40 psi, and that the venturi generates 5 psi additional pressure. The actual exit orifice pressure is now only 15 psi. This is at the lower limit at which a spray is atomized, and at which a good pattern can form.

    Our general recommendation with venturi-style low-drift tips has been to avoid pressures below 30 or 40 psi for that reason. We’re trying to prevent the spray becoming too coarse for adequate coverage, and also to prevent the spray pattern from collapsing.

    The upside of this design is that the same principle allows for much higher-pressure operation without creating excessive drift. These types of nozzle can, in fact, be operated at 70 to 90 psi without becoming very drift-prone because the pressure at which the spray liquid is atomized is likely only 30 or 40 psi (the actual exit pressure and drift potential will depend on the nozzle and the formulation).

    Speed Range

    A low-drift nozzle with a pressure operating range from 30 to 90 psi (i.e., 3-fold) would have a flow rate range of 1.73 (i.e., the square root of 3 due to the square root relationship of flow rate and spray pressure). This means that the fastest travel speed (at 90 psi) would be 1.73 times the slowest travel speed (at 30 psi).

    A conventional nozzle operating between 20 and 60 psi would have the same travel speed range. So why don’t we just do that? The main reason is that the two-stage design lowers the overall amount of drift substantially, something a conventional nozzle can’t achieve even at very low pressures.

    A second reason is that even at high pressures, a two-stage design will likely drift less than an conventional nozzle. This is still the case if the conventional nozzle is operating at low pressures. Any spray quality chart comparing spray qualities of conventional and low-drift tips will demonstrate that.

    Pulse Width Modulation

    PWM uses a solenoid to intermittently shut off nozzle flow, between 10 and 100 times per second (Hz) depending on the manufacturer. This has implications for nozzle design because the nozzle must not leak liquid during the brief off-cycle. If it does, the small amount of liquid leaving the nozzle will not only not atomize properly, it will also cause a pressure drop within the nozzle which must be replenished with the next on-pulse. This will mean the on-pulse will operate at a lower initial pressure, affecting pattern development and atomization. For this reason, venturi-style low-drift nozzles have not been recommended with PWM. The venturi provides an alternate exit for air or liquid, compromising nozzle performance.

    And yet, some venturi style nozzles do, in fact, produce acceptable patterns with PWM according to the nozzle manufacturers. This goes to show that nozzle design can continue to evolve to provide the best in drift reduction technology with PWM. Design for PWM suitability should be at the top of nozzle manufacturers’ agendas.

    Nozzle design continues to evolve. But in the foreseeable future, spray pressure will continue to control pattern width and droplet size. That’s why understanding the pressure limits of any specific nozzle type, and maintaining pressure within those limits, is so important in any spray operation.

  • Exploding Sprayer Myths (ep.7): Boom Height

    Exploding Sprayer Myths (ep.7): Boom Height

    It’s a new season of Exploding Sprayer Myths so we’ve got a new opening sequence!

    In this episode we demonstrate the importance of nozzle spacing, spray angle and boom height. We also turn a hapless pineapple into a projectile and spray dyed antifreeze on a cold winter day.

    Learn more about how boom height affects spray deposit uniformity, and why that should concern you, by going here.

    This episode was filmed on location at the Syngenta Honeywood Research Facility in Plattsville, Ontario. We thank them for generously allowing us to commandeer their facility and staff for the day.

    And of course, none of this would be possible without the talented staff at Real Agriculture. Make sure you tune into RealAg radio.

    A little extra fun:

    We received this email after a grower heard Tom speak at a meeting. A compelling observation about how nozzle spacing and drift affects men everywhere:

    Tom: I really enjoyed your talk in Humboldt yesterday. During the coffee break immediately after, I went to the washroom and noticed 3 guys spread evenly across 5 urinals. Wow. Talk about worrying about spray drift. When I returned to my table and told my wife of my findings, she commented that it must have something to do about the distance to the target, as it couldn’t possibly be that the pressure was too high!

  • Three Features that Should be Standard on all Sprayers

    Three Features that Should be Standard on all Sprayers

    One of my main activities in the winter is public speaking. Attending producer meetings gives me the privilege of meeting many farmers, learning about their operations, and sharing my research results.

    I enjoy providing practical solutions to problems. But there are three issues that always come up to which I wish I had better answers. Here they are:

    1. The Correct Spray. We’re stuck with compromises in this area. We need small droplets for coverage. We need large droplets for drift control. We need to keep application volumes moderate for productivity. We’ve basically asked the nozzle to shoulder the entire burden of our application needs, seeking a spray that hits all the right notes. Not too fine. Not too coarse. Able to work with fast and variable travel speeds and high, variable boom heights.

    Based on our research in field crops such as wheat, canola, corn, lentils, etc., we can be confident that Coarse, even Very Coarse sprays, coupled with a reasonable water volume, are appropriate for most modes of actions and target situations. These sprays contain enough small droplets for good coverage, and their larger droplets work surprisingly well in most cases. Sure, a finer spray could save some water. And a coarser spray would reduce drift even more. But we need a compromise spray, combined with some lucky weather, to get the job done.

    And yet we usually make spray quality recommendations with caveats, because droplet size alone isn’t enough. Drift is always a possibility, no matter how coarse we go. Coverage is not guaranteed, especially if the canopy is dense. Finer sprays will get deeper into a broadleaf canopy, but then we may have drift or evaporation to deal with.  The nozzle size, volume, and travel speed relationship has to be just right so the spray pressure is in the correct range. And on it goes.

    I’d like to give the overworked nozzle some help. We used to use shrouds to protect fine sprays from drift. Now it’s time to let air assist take over that task.

    Air assist booms can accelerate (i.e., add kinetic energy to) small droplets so they’re less prone to off-target movement. Properly adjusted, air assist can carry these droplets deeper into the canopy and enhance their deposition.

    A good air-assist system allows the user to select the strength and direction of the airblast to match canopy, boom height, and travel speed conditions.

    Air assist is the workhorse of most fruit-tree and vineyard spraying.  It has to be done right to provide all the benefits I mentioned, and certain approaches should be rejected. For example, there are some companies using air assist to promote very fine sprays with very low volumes. That’s the wrong use of the technology, and invites a backlash.

    Instead, we need systems that work with existing spray practice to address some of its classic shortcomings, such as drift management, deposit uniformity, and canopy penetration.

    Let’s see some products. It’s time to bring air-assist to the mainstream of agricultural spraying.

    1. Boom Height, Level, Sway and Yaw Control. Boom height is so fundamental it’s almost boring. We’ve long said that it’s important to set the boom at the right height for proper nozzle overlap and drift control. It was easy with wheeled booms. But over the last 15 years, suspended booms coupled with fast speeds have caused booms to rise again (RISE OF THE BOOMS!).

    Fact is that there are some tasks we’re asking of nozzles that they simply can’t achieve without level, low booms. Drift control is one such thing. Low booms are surprisingly effective at reducing drift, not only because winds are lower closer to the canopy, but also because droplet velocities are faster closer to the nozzle.

    Angled sprays for fusarium headlight control are another thing that is more effective with low booms.

    Spray droplets released from an angled spray soon slow down and get swept back by air resistance and begin to fall vertically, or move with wind currents, reducing their intended benefit. Low booms can prevent that.

    Uniform and low booms also keep deposit variability more manageable. They can save energy needed for air-assist systems. The shorter the path to the target, the less air-velocity will be needed to get it there.

    So how about it? Can we have boom linkages and suspension systems, coupled with sensors and hydraulics, that are stable and maintain 20” above canopy at 16 mph on uneven ground? Can we have systems that do this reliably enough that we’re prepared to invest in, say, expensive nozzle bodies? It’s possible.

    1. Sprayer Cleanout. One of my favourite questions about cleanout is: “When do you know that you’re finished cleaning the sprayer tank and booms?” Inevitably, someone from the back yells: “In two weeks!” And we laugh, knowingly.

    We have a terrible system of sprayer decontamination. It’s a process that is awkward, imperfect, and time consuming, often leading to poor practice. I’ll ask a group of producers what they do with their pesticide waste. The response is silence. I don’t blame them for not telling me that they dump the remainder on the ground somewhere, but I’d rather they didn’t. Sprayer designs don’t help.

    What we need is a system that guarantees results. To start, a tank gauge that is reliably accurate to the nearest gallon would remove some of the filling guesswork and help minimize leftovers.

    We need a remainder volume (volume left in the non-boom plumbing after the pump sucks air) that is known and small, because that remainder can’t be expelled and needs to be diluted. The smaller it is, the easier it is to dilute.

    We need pumps that can run dry, so nobody has to fear spraying the tank out completely.

    We need a wash system that requires little volume and works quickly, like continuous rinsing.

    We need plumbing that is easy to understand and whose inside surfaces do not absorb pesticide, or hide it in corners and dead ends. Perhaps it’s a recirculating system. Perhaps it hasn’t been invented yet.

    We need pesticide formulations that clean up easily. We need an easier way to inspect and clean filters. And we need a safe place to put any waste that can’t be sprayed out in a field.

    I’d like to see a sprayer that can be decontaminated in 10 minutes without the operator leaving the cab, and without any spillage of spray mixture. Clean enough to spray conventional soybeans after a tank of dicamba. Clean enough to spray canola after a tank of tribenuron. I know it’s possible.

    I also know what many of our European readers are thinking right now. Much of what I’ve discussed exists in the EU in some form or another. Why does the North American, and to a lesser extent the Australian market, not have these features?

    Part of the reason is federal standards and regulations. Some European countries test and approve products for remaining tank volume, boom stability, and spray drift, for example. Others have sprayer performance criteria that must be met to be eligible for sale in that country. An increasing number have mandatory sprayer inspection.

    These requirements serve to protect the producer and the environment. They’re an example of useful government actions. Despite, or perhaps because of, stricter rules, the entire EU marketplace is very competitive, with about 75 sprayer manufacturers. Bottom line: producers benefit.

    We need leadership, preferably from a combination of government, industry, and producers, to achieve better sprayer designs. Our market has room for products that make it easier to prevent drift, protect water, and protect yields.

    As they say, a rising tide lifts all boats. And it will certainly make my job easier.

  • Spray Drift – Why is it still happening?

    Spray Drift – Why is it still happening?

    Despite the abundance of information available on spray drift, we continue to see widespread incidents of damage to a variety of crops every year. Do applicators just not care or are they missing some vital information when making decisions to spray? I believe it is the latter.

    What is the problem?

    In my experience, the vast majority of spray drift cases (probably 90% or more) are the result of ‘inversion drift’. That means the drift has not come from an adjacent sprayed area, it has come from one or more sources that are some distance from the site of damage. The distance between the sprayed site and the location of the damage may vary dramatically, from a few kilometres to tens of kilometres.

    Why is there so much inversion drift when labels specifically prohibit use of the products under surface temperature inversions? Many may argue that it is a blatant disregard of the label by a few applicators (translation = cowboy operators). I do not agree this is the main problem. While I can confirm the existence of ‘cowboy operators’, thankfully they are limited in number. I believe the problem is a lack of understanding about how to tell when there is an inversion and particularly not knowing how ‘day wind’ moves differently to ‘inversion wind’. I continue to see good farmers/applicators doing what they believe to be the right thing but it is not. These are people very concerned about minimizing spray drift; they honestly do not think they are doing anything wrong.

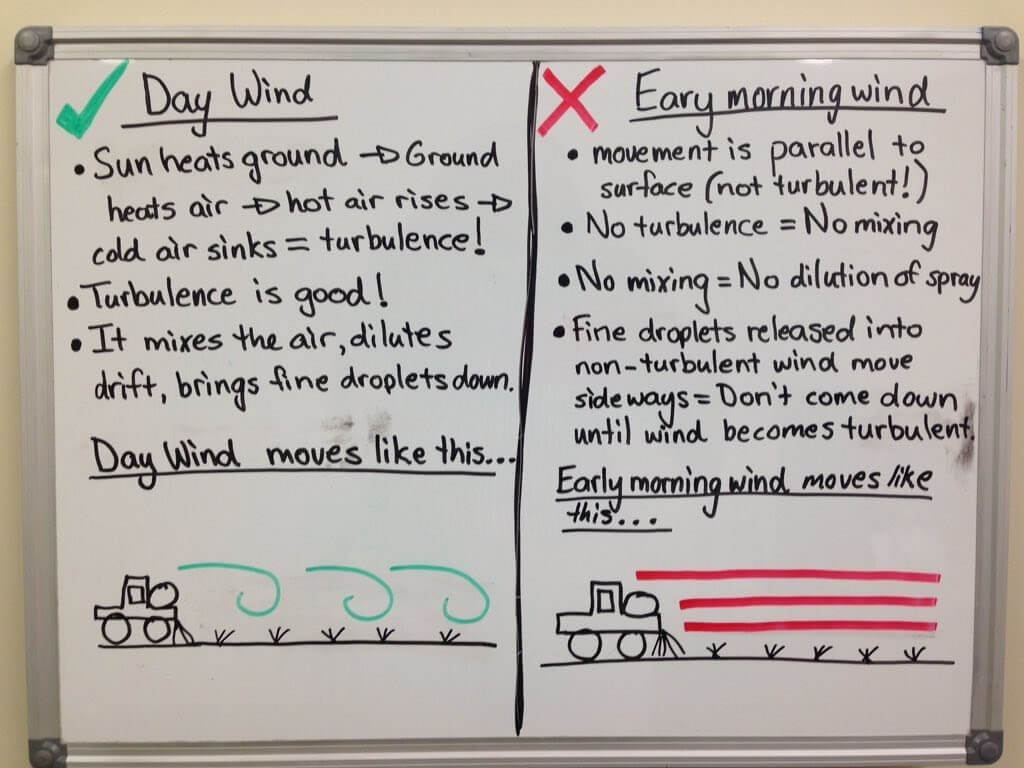
    What is ‘day wind’?

    After sunrise, the sun begins to heat the ground, the warm ground then heats the air close to the surface, and this air then rises. As that warm air rises, cold air from above sinks down to replace it. The ground then warms this cold air and it rises. This cycling of warm air rising and cold air sinking creates turbulence and then wind. This is a good thing; turbulent wind movement is much safer for spraying. ‘Day wind’ has a turbulent motion and is much more likely to pull any fine droplets to the ground within a reasonable distance. During the day, we can predict which direction and how far our fine droplets will travel.

    What is ‘inversion wind’?

    As the sun sets, the ground begins to cool quickly and this in turn cools the air next to the ground. As we all know, cold air does not rise and warm air does not sink. This means there is a layer of cold air trapped close to the surface and a layer of warm air above it. The result is no turbulent movement or mixing of the air. The air may become quite still and this is often observed around sunset when the daytime wind ceases or drops off. What happens next is where the real danger occurs for spraying.

    As the night progresses and the ground cools more, the cool air close to the surface becomes colder and therefore more dense, particularly from midnight onwards. This cold dense air then begins to move across the landscape, often down slope and in very unpredictable directions. Remember this air is not turbulent, there is no mixing, it has layers of air, something like layers in plywood, and it flows parallel to the ground. Any fine droplets released into these layers of cold non-turbulent air will simply move sideways across the surface until the sun rises and heats the ground again. This is when the fine droplets are released from the layers and they come to ground, often in the lower parts of the catchment and a long way from the site of application. It is impossible to predict what direction this ‘inversion wind’ will go. For this reason, spraying in this type of wind is extremely high risk for spray drift.

    Key indicators that and inversion is unlikely

    • We should always expect that a surface temperature inversion has formed at sunset and will persist until sometime after sunrise unless we have one or more of the following: continuous overcast weather, with low and heavy cloud;
    • continuous rain;
    • wind speed remains consistently above 11km/h for the whole time between sunset and sunrise;
    • and after a clear night, cumulus clouds begin to form.

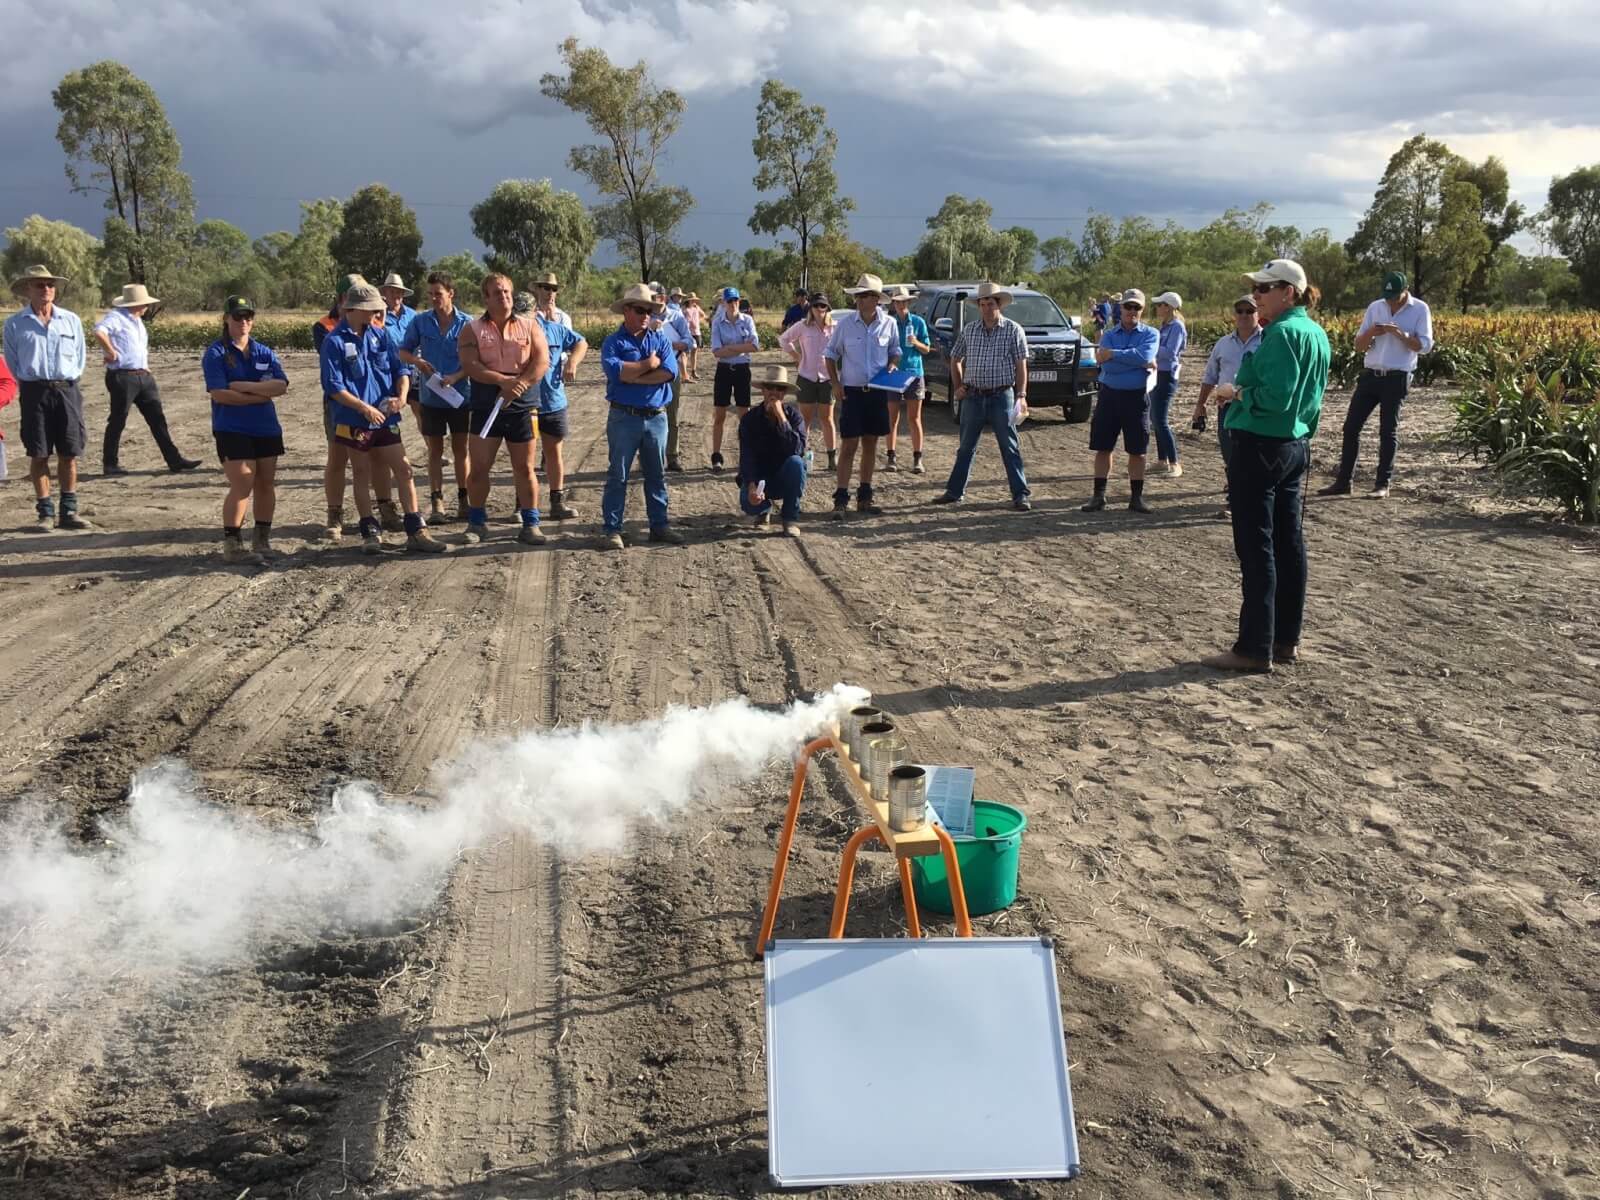
     Inversion wind movement – practical demonstration video

    Wind is a key factor in any spray application. The problem is that not all wind is the same. To reduce the incidence of spray drift, it is critical that spray applicators understand how wind moves, particularly during a surface temperature inversion. This video uses smoke flares to visually demonstrate the air movement under inversion conditions.

    Here’s what we’re looking for: moderate wind with consistent direction that disperses spray and drives it to ground.

    Conclusion

    Many factors affect the potential for spray to drift but the main ones are; the weather conditions at the time of application, nozzle selection, products/tank mix used, actual spray quality achieved, speed of rig, and boom height. The common denominator is that all of these things are within the control of the spray operator.

    Spraying under inversion conditions is extremely high risk and prohibited on many product labels, that means it is illegal. If you are serious about preventing drift, then you must learn how to identify when an inversion is likely to be present and more importantly when it has broken.

    All agricultural chemicals have the potential to drift; it is how we use them that increases or decreases that potential. Therefore, the problem is a human one, not a chemical one. There is a suite of information available but if you are still unsure or need any assistance, please seek advice from an expert. Maintaining long-term access to key products depends on us reducing spray drift.