Author: Tom Wolf

  • What is Spray Quality, Part 2 – Describing Sprays

    Hydraulic atomizers comprise the majority of agricultural nozzles. They work by forcing a liquid through an orifice, resulting in a liquid sheet that is inherently unstable. The sheet breaks into ligaments and eventually droplets within a few centimetres of leaving the nozzle. The physico-chemical properties (elongational viscosity, dynamic surface tension, etc.) of the liquid affect the shape of the sheet and its stability, and therefore play a role in atomization.

    The dimensions of the liquid sheet depend on the nozzle type and the conditions in which they release the liquid. Flat fan nozzles, the most common in agriculture, force the liquid through an elliptical orifice that results in a sheet that is thicker in the middle and tapers at the edges. Nozzles that produce wider fan angles have narrower orifices, creating thinner sheets that ultimately produce finer sprays. Higher flow rate nozzles produce thicker sheets. A deflector nozzle impinges a stream of liquid against a plate that forces the stream flat and spreads it out, creating a different set of forces that destabilize the sheet. A cone nozzle generates a swirling action that results in a less stable sheet.
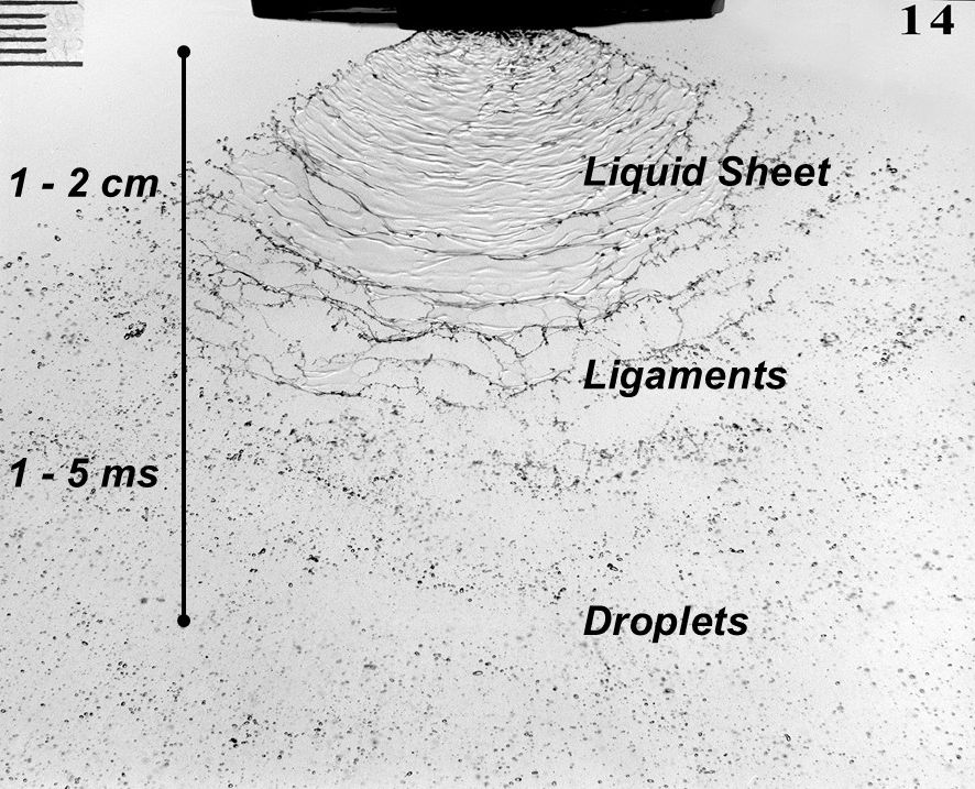
    Fig. 1: Three stages of hydraulic atomization of a flat fan nozzle. A sheet emerges from the exit orifice, which becomes unstable, forming ligaments that ultimately break into droplets (Image Source believed to be Silsoe Research Institute)

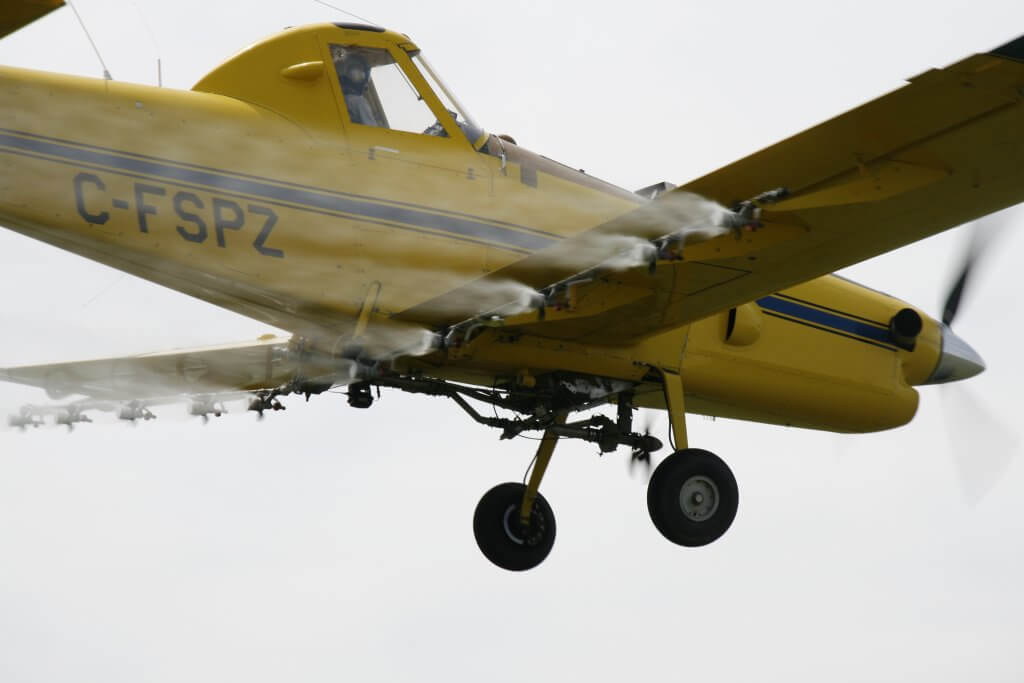
    If we place these nozzles into an airstream, either from travel speed or ambient wind, the spray sheet will become less stable and result in finer sprays. The amount of air-shear atomization will depend on the relative orientation of the nozzle sheet and the moving air. Nozzles that spray parallel to moving air produce less air shear and therefore result in coarser sprays than nozzles oriented perpendicular to the air stream. This characteristic is exploited by aircraft as a means of droplet size control, having a greater effect than spray pressure. 

    Rotary atomizers, either from rotary cages or spinning disks, are capable of producing sprays whose droplet size ranges are more uniform than those from traditional hydraulic atomizers. This produces advantages ranging from improved drift management to better use of available carrier volume. Rotary atomizers are popular with aerial applicators and are found on the majority of spray drones.
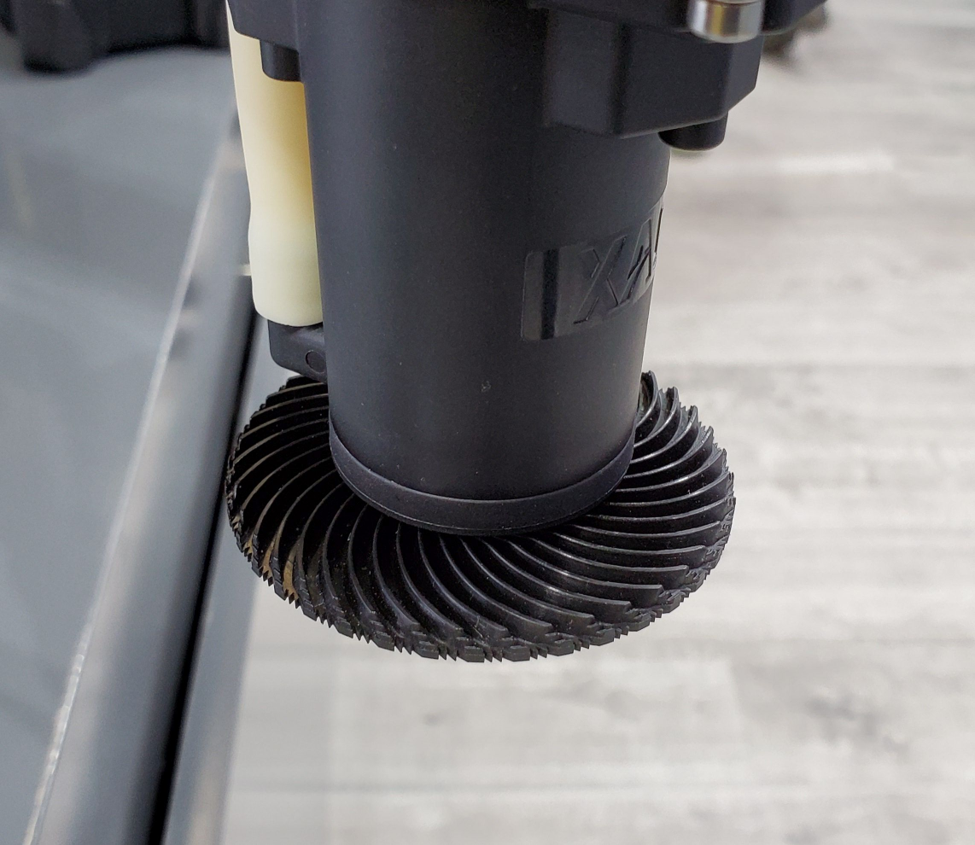
    Fig. 2: Rotary atomizer on a spray drone. Water is moved to the edge of a serrated disk by centrifugal force, forming ligaments that break into droplets

    Rotary atomizers create finer sprays when their rotational velocity is increased, or when the flow rate of the nozzle is decreased. In both cases, the ligaments formed at the periphery of the atomizer are thinner and will break up into smaller droplets. One disadvantage of rotary atomizers is the limited flow rate that they can atomize. For high flow rates, rotary cages, which break up the spray liquid by passing it through a series of wires mesh stages, are used. These require a fair amount of power, making them impractical for most smaller drone sprayers. 

    Droplet size ranges

    All hydraulic agricultural sprays are said to be polydisperse. This means that they are made up of a number of droplet sizes ranging from perhaps 5 µm to 1000 µm, or even 2000 µm or more for low-drift nozzles. How should the spray cloud be described?

    The vast majority of droplets in hydraulic sprays are small. In any sample of flat fan nozzles, low drift or not, about 80 to 90% of the total number of droplets will be less than 150 µm in diameter. This held more or less true for a wide range of nozzles. As a result, using a traditional weighted average droplet diameter was not useful as a descriptor because the abundant sizes would always control the outcome even though they contained a minority of the spray volume. The contribution of the larger, but less abundant droplets would be hidden with an arithmetic mean.

    Any other descriptors based on droplet number alone, such as mode (the most frequent size class) or median (the size class above and below which were an equal number of droplets) are equally dominated by the high abundance of the smaller droplets.

    To solve this problem, droplet diameters can be converted to their volume equivalent using the formula
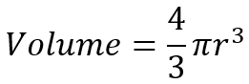

    Where r is the radius of the droplet.

    This is relevant because the dose of pesticide in a droplet is related to its volume. It’s important to understand the contribution of relatively few larger droplets in terms of how this dose was received by plants.
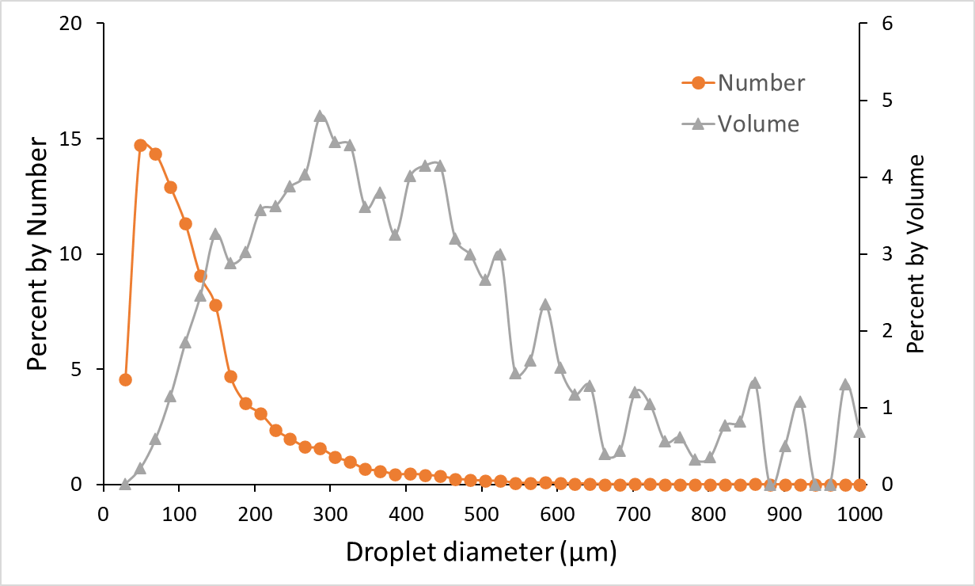
    Fig. 3: Number and volume distributions of a typical agricultural spray (Wilger SR11005 @40 psi)

    Thus we arrive at a volumetric distribution, where each diameter is described by the proportion of the total spray volume it represents. That volume represents the dose of spray. Now we have some practical meaning of the numbers.

    First we generate a cumulative volume distribution. The volume contained in each size fraction is expressed as a percentage of the total volume and these are added together.

    The cumulative distribution can now be divided into benchmark values so we can get values that differentiate various sprays. The key ones of interest are the 10th, 50th, and 90th percentile. The 10th percentile, known as the DV0.1, is defined as the diameter below which is 10% of the total volume of the spray. DV0.5 and DV0.9 likewise describe the diameters below which are 50% or 90% of the spray volume, and the former is more commonly known as the Volume Median Diameter (VMD). Recall that the median is the value that divides a distribution in half by number, therefore the 50th percentile is also the median.
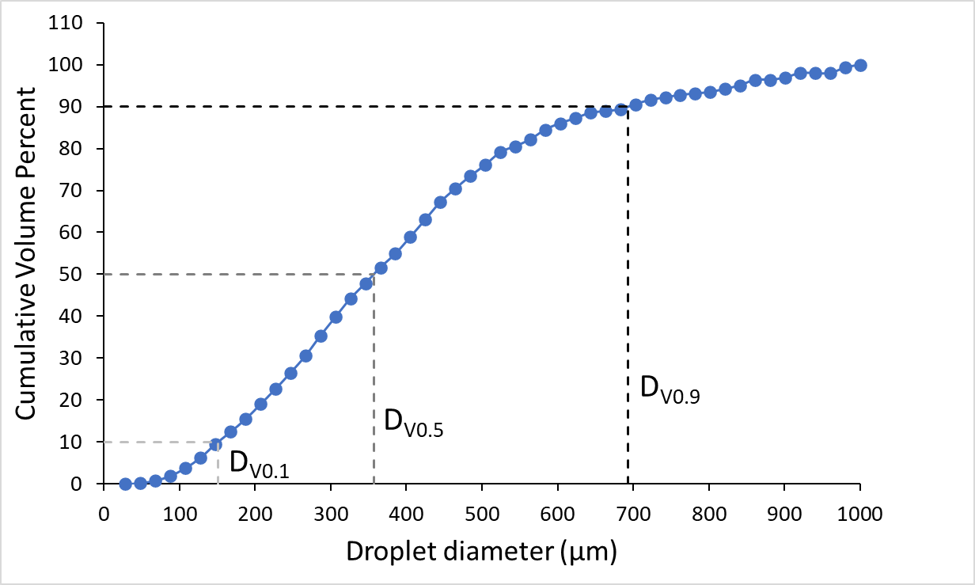
    Fig. 4: Cumulative volume distribution of Wilger SR11005 @ 40 psi. Dashed lines show DV0.1, DV0.5, and DV0.9.

    The VMD is the benchmark value, it can be thought of as the diameter near which the majority of the dose is delivered. The DV0.1 can serve as a drift index, describing the diameter that contains the smaller droplets. Sprays that are more drift-prone have lower DV0.1 values. The DV0.9 can be an index of the droplets that may not be able to contribute much to product efficacy because they are too big to cover much area, and they are likely to be very rare, possibly missing the target altogether. Higher DV0.9 values indicate that more of the spray may be lost to large droplets that will likely rebound.

    All of these parameters are related to each other. A finer spray will have lower DV0.1, DV0.5, and DV0.9 values. But it is not necessarily correct to say that a spray with a lower DV0.5 will have less drift potential. Some nozzles, by virtue of their design, can have smaller driftable size fractions as well as a lower DV0.5.

    There are other parameters that one may encounter during droplet size measurements. One is the Relative Span, which describes the uniformity of the droplet sizes in a spray. A perfectly uniform spray (containing droplets that are all the same size) will have a span of 0 because all three volumetric parameters will be equal.


    We sometimes encounter the Sauter mean of a spray, which can be defined as the diameter of a drop having the same volume/surface area ratio as the entire spray. This is useful when surface area is of importance, such as in combustion or evaporation.

    The popularity of laser measurement systems, and their ability to measure droplets that previously escaped detection, was a boon to the spray industry. But it quickly became clear that simply comparing these parameters was problematic. Each laser system, and indeed each laboratory that used them, seemed to create their own unique values for the same nozzles. We will explore the solution to this problem in Part 3.
  • What is Spray Quality, Part 1 – Measuring Droplet Size

    What is Spray Quality, Part 1 – Measuring Droplet Size

    It’s often been said that droplet size is the most important factor governing spray operation success. Both spray drift and pesticide efficacy depend to a large degree on droplet size. For something this important, the droplet size information from nozzles ought to be accessible and easy to understand. 

    There are a few problems to overcome before we get there.

    The first is the difficulty in measuring droplets in the first place. Spray droplets are very small and evaporate quickly.  In the early days of spray technology research, sprays would be captured on a surface and individual droplets measured and counted under a microscope. A common approach was to use magnesium-oxide coated glass slides. The magnesium oxide layer was soft, and an impinging droplet left a tell-tale crater behind, much like those found on the moon’s surface. This allowed the analysis to be done after evaporation. Magnesium oxide does a great job but relies on droplets having enough momentum to leave their mark. There is also a spread factor (ratio of crater diameter to droplet diameter) that has to be known.

    Water-sensitive paper (WSP) is the modern version of this concept, and we’ve written much about the topic. Jason in particular has done a deep dive on how WSP works and how it’s analyzed.

    We can also add dye to spray mixtures to see deposits on various glossy paper surfaces.  The resolution of the dye-droplets can be better than those from WSP but their deposits can also be so faint that they pose thresholding and analysis problems.

    The great thing about impingement methods like WSP is that they’re easy to use, and they are particularly useful for a quick visual and qualitative assessment of coverage. If wanted, coverage can be quantified by scanning the WSP for percent area covered or deposit density.

    Droplet size determination is problematic on WSP because one needs to know the spread factor (how much larger the deposit is compared to the in-flight droplet that caused it) to back-calculate the original size of the in-flight droplet.

    Spread factor depends on droplet size, velocity, formulation, and the nature and orientation of the surface it’s collected on. The SF formula provided by the paper manufacturers is a good start but it is far from perfect.

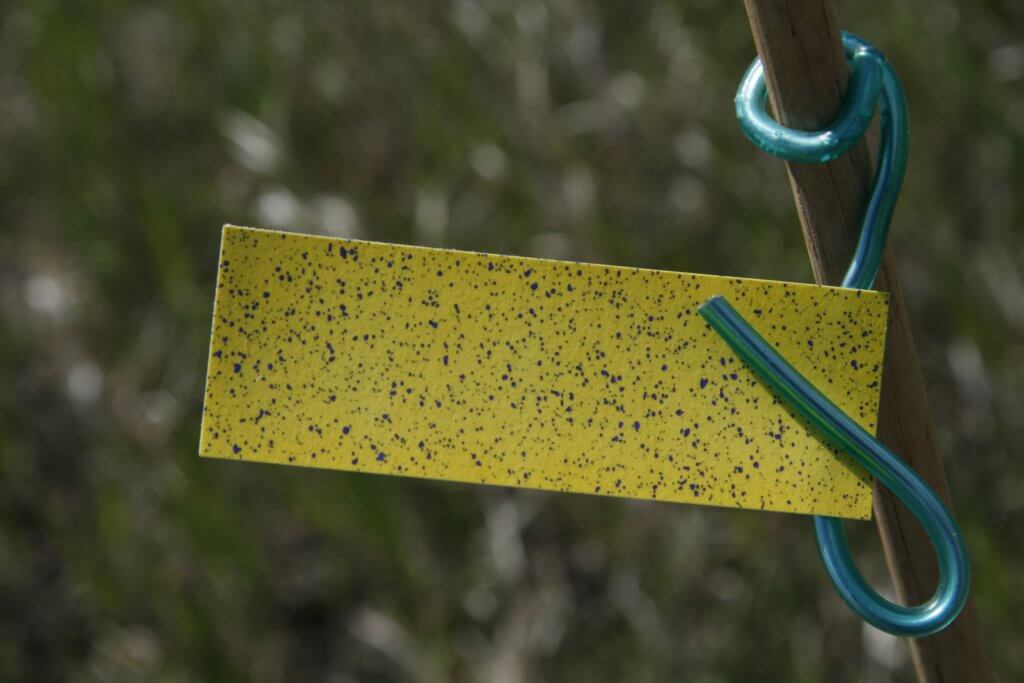
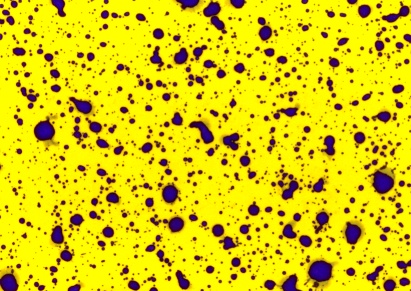
    Fig. 1: Water-sensitive paper (WSP) treated with a Very Coarse spray at about 100 L/ha. Note the coalescence and overlap of some deposits.

    In addition, the overall droplet density has to be low enough to avoid overlaps or coalescence. Usually a water volume over 50 to 100 L/ha will create issues. The WSP also has to collect the droplet in the first place. Smaller droplets often move around larger objects such as a leaf, or a similar sized piece of paper. If they impact at a sharp angle, the deposit will be elongated due to smearing and that creates additional difficulties.

    Even if the paper collected the smallest droplets, they may not appear as stains. Droplets below a certain diameter (about 50 µm) do not leave a visible deposit on the paper. 

    So, while WSP is a great tool for visualizing a deposit, its limitations usually prevent it from being used to accurately measure the droplet size spectrum of a spray. 

    The Rise of the Laser

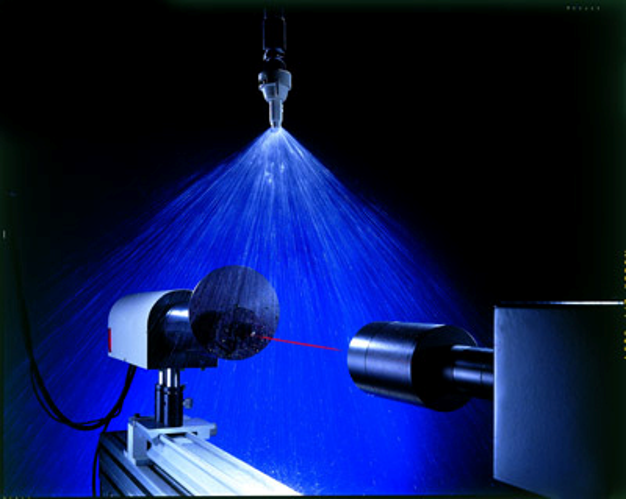
    In the 1970s and 80s, we saw the introduction of laser-based droplet size measurements. With these, a spray simply needed to be directed into a such an instrument, and it very quickly determined the diameter, and in some cases, the velocity, of the droplets. The principles employed by various laser instruments differed, and although one could now rapidly obtain data in-situ, the numbers among the instruments didn’t always agree.

    Fig 2: Laser instruments help to measure droplet size of sprays (photo source: TeeJet)

    The Most Common Laser Systems

    Laser diffraction: One of the first droplet sizing instruments is manufactured by Malvern (https://www.malvernpanalytical.com/en), and is still in use today. A laser beam passes through a spray cloud. The system uses a laser diffraction principle that works as follows, according to Malvern: “Large particles scatter light at small angles relative to the laser beam and small particles scatter light at large angles. The angular scattering intensity data is then analyzed to calculate the size of the particles responsible for creating the scattering pattern, using the Mie theory of light scattering.”

    To calculate the droplet sizes responsible for the scattering behaviour, the laser system has light-sensitive sensors in concentric circles behind the spray plume. When a sensor in the middle of these rings picked up a signal, it likely originated from a larger droplet because of its lower light scattering properties. Sensors further from the centre picked up smaller droplets. The system thus had an idea of the relative frequency of the various droplet sizes in the spray cloud and modelled these according to the classic Rossin-Rammler spray distribution model, from which descriptive parameters are calculated.

    Laser diffraction is the most popular method for in-situ droplet sizing. The company Sympatec (https://www.sympatec.com/en/) also offers a system that competes with Malvern that is found in many labs.

    Laser Shadowing: The Particle Measuring Systems (PMS) system was one of the earliest laser systems. It was a very compact and sturdy system that shone a laser light at the spray cloud and the droplets in that cloud cast shadows against a sensor array a fixed distance away. The size of these shadows could then be measured to arrive at a droplet size distribution. The PMS was particularly good at measuring small droplets.

    Although long discontinued, the PMS system had the basic appearance of a torpedo and was often mounted on aircraft or in wind tunnels to measure cloud aerosol sizes. Very cool. The company still manufactures other particle measuring devices (https://www.pmeasuring.com/).

    Pulsed Laser Illumination: This is a different approach to the laser shadowing of the PMS system. Oxford Lasers systems (https://oxfordlasers.com/) use a video camera to view the spray cloud and freeze images from using a very high frequency pulsed laser light. This light illuminates the cloud briefly which allows a still image to be briefly displayed.  Image analysis then measures the diameter of each particle in the image, adjusting for out-of-focus images.  It’s possible to analyze the speed and direction of the particles by comparing the particle position in subsequent images. This system is quite popular among scientists due to its ease of use. A portable unit that can be deployed in fields is available.

    Phase Doppler: In the mid 1980s, a system was developed that uses the Doppler principle to measure both the speed and diameter of droplets. Two out-of-phase laser beams intersected in a spray cloud, and a droplet passing through the intersection point created a Doppler burst that signalled the speed of the droplet. The burst signal also contained information on the droplet diameter, derived from a frequency shift of the two laser beams utilized in the system. This system has very high data acquisition and was the first to create a temporal sample of the spray, increasing the accuracy of the droplet size measurements.

    Initially brought to market by Aerometrics (later acquired by TSI) and called the Phase/Doppler Particle Analyzer (PDPA), it is now mainly offered by Dantech systems (https://www.dantecdynamics.com/).

    Sampling Bias: Temporal vs Spatial

    It’s not straightforward to measure a sample of moving objects. It may seem intuitive that if one wants to know how many objects are present, taking a picture and counting the objects would provide the answer. But when objects move at different speeds, that answer will be incorrect because the slower moving objects will be over-represented.

    Let’s assume you’re working on a traffic count project to understand the number of people crossing a bridge either walking or cycling. Let’s also assume that one walker and cyclist depart for the bridge every 5 seconds, i.e., there are the same number of each. If you wait until the bridge is full of people crossing and take a picture it will show more people walking on the bridge than riding bicycles. That is because the bicycles are faster and many will already have left the frame.  Thus counting the number of people in the picture over-estimates the number of walkers because they move slower.

    The same problem arises with these laser systems because in a hydraulic spray, the smaller droplets move slower than the larger droplets. Any system that takes a picture and counts what’s in it will have what’s called a spatial sample, overestimating the slower (smaller) droplets.

    A temporal sample can measure the velocity of the droplets and therefore account for their speed, giving a more accurate measure of the abundance of the droplets. In the case of the PDPA, it acheives this simply by counting all the individual droplets that pass, in sequence, through its meassurement area, called the probe volume. As they pass, it notes their velocity and diameter.

    To address this issue with a spatial sampling instrument, many labs now use wind tunnels and direct the spray to be tested with the wind direction. This forces the droplets to move at more or less the same velocity as the wind, eliminating or at least minimizing the speed differences before the droplets reach the laser instrument.

    WSP produces a temporal sample because it ultimately catches all droplets, but it has different types of sampling bias. Large deposits usually cover smaller ones. Smaller droplets may not impact on the target due to poor collection efficiency. Small droplets may dry too quickly to leave a visible stain. As a result, even if we had accurate spread factors, we would tend to under-estimate the number of smaller droplets, opposite of the error of spatial systems.

    Scanning the pattern

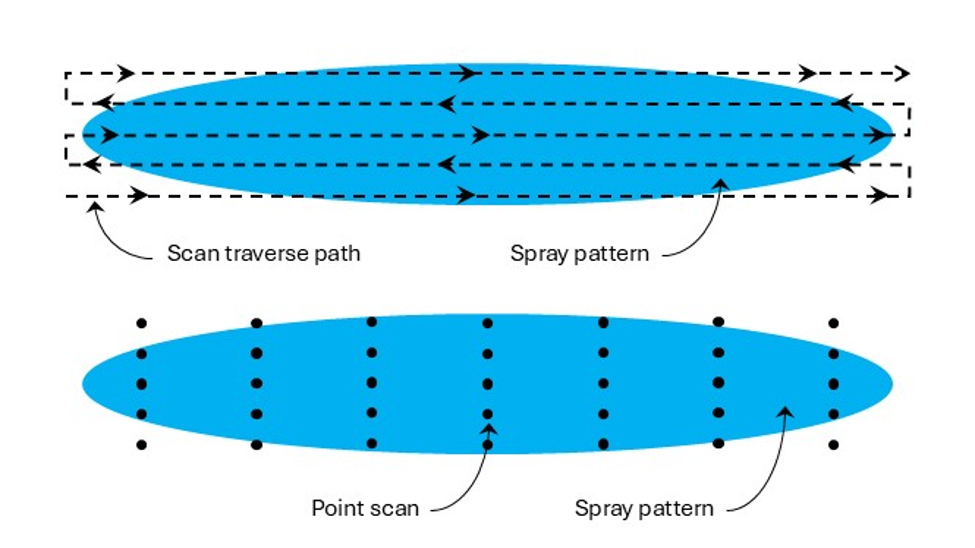
    Droplets are not distributed uniformly within a spray pattern. In a flat fan nozzle, for example, the centre of the pattern contains the smaller droplets. The outside edges of the pattern contain fewer small droplets and more large droplets. Some laser systems have a very shallow depth of field, and the PDPA is a point-measurement. As a result, it is not accurate to simply point the measuring device at a single location of the spray pattern. Accurate droplet size spectra from lasers requires a thorough traversing scan of the spray pattern along at least its long axis, and preferably two or more such traverses at increasing distances from this central axis. The scanning method would likely need to be adjusted to suit various types of atomizers, such as hollow cone nozzles.

    If no traversing mechanism is available, it is acceptable to measure the spray at several discrete locations and then merge the data prior to analysis. In all cases, three replicate samples should be taken so that an estimate of variability is available.

    Many labs, having compared a full scan with many traverses to those with fewer traverses have opted for a simple back and forth traverse with little loss in accuracy.

    Fig. 3: Possible ways of scanning a spray pattern for droplet size analysis. Top: traversing scan. Bottom: point scan

    Sometimes sprays are atomized within a chamber to prevent the droplets from contaminating the surrounding area if they contain any active ingredients. These chambers can also add measurement errors from, say, small droplets that recirculate within the chamber, or due to any glass surfaces through which the laser lights must pass. These all need to be considered, as they add to the many variables that create different results even when comparing identical sprays between labs.

    The next topic, covered here, is how to use the information we gather from droplet measurements. As you might expect, this is also not as straightforward as it seems.

  • Sprayer Productivity for Smaller Scales

    Sprayer Productivity for Smaller Scales

    Travel is an amazing teacher. It exposes assumptions and replaces them with real life experiences.

    On a recent trip to New Zealand, I learned a valuable lesson in sprayer productivity. I had long talked about wider booms being a key factor, being an easy change that allowed more area to be covered per pass. I had assumed large fields, large tanks, and fast fills as part of that system, and validated it with calculations and observations.

    During that trip, I learned that things look really different when the landscape dictates certain limitations. In places like New Zealand, fields tend to be smaller, as expected, with the longest run averaging 300 m or so. Sprayers are also smaller capacity, with trailed sprayers typically fitted with a 24 m boom and a 3000 L tank. Mounted sprayers, commonplace on the North Island, may have smaller tanks and booms, with 2000 L and 18 m width a reasonable average. Self propelled sprayers are not common on farms, but custom applicators use them.

    Tender systems (called bowsers) are also rare. Most applicators return to the farm yard, or another nearby water source, to fill. A single filled sprayer can often do that entire field, so moving to a new field and re-filling are part of the same workflow.

    Some very interesting things happened when such a scenario was analyzed.

    We used a newly re-vamped Productivity Calculator (below) to make the calculations.

    Some basic configurations were assumed. All sprayers travelled 15 km/h when spraying, and turned in one headland at 8 km/h. The tank remainder that necessitated a re-fill was set at 5% of tank volume. Tank cleaning was assumed to be required every four tanks, taking 60 minutes. Sprayers were typically refilled in the farm yard or a nearby water source, requiring a ferry (transport) time of 15 minutes each way.

    The first scenario was the base configuration, from which one factor was changed in each iteration to examine the magnitude of the change. With the 24 m boom, 3000 L tank, 200 L/ha application volume, a field length of 300 m, a loading time of 30 minutes, and a loading location that required a 30 minute round trip, net productivity was 8.0 ha/h. 22% of engine hours were spent spraying, the remainder was lost to turning at the end of a run, driving to the loading location, loading the sprayer, and cleaning it. We will call that the spraying efficiency.

    Because wider booms are successful in improving productivity in western Canada, we examined the practice for smaller farms. Increasing the boom width from an average 24 m to 36 m yielded the first surprise. Productivity only increased to 8.5 ha/h (7%), and spraying efficiency was reduced to 16%.  The problem appeared to be that the wider boom dispensed with the tank contents faster, requiring more frequent filling. And that of course was the big time user, accounting for 60% of the engine hours. 

    The next step was to examine a larger tank (5000 L), keeping the original 24 m boom. This change yielded big results, with productivity jumping to 11.1 ha/h, a 33% increase from the base condition. The larger tank reduced the frequency of filling, and that reduced its drag. Spraying efficiency jumped to 31%.

    Another way to achieve a lower filling frequency is to lower the amount of water applied. This is a bit risky, as water volume is likely to most important variable that ensures good spray success, especially when dealing with dense, high yielding crop canopies. In cases where canopy penetration isn’t an issue, and systemic products can be used, less water may be an option. A modest decrease from 200 to 150 L/ha was tested.

    Again, a large jump in productivity was observed, from the base of 8.0 ha/h to 9.7 ha/h, about 21%, resulting in 27% spraying efficiency.

    What if fields were merged, or shelterbelts removed, resulting in longer spray passes? These would reduce the time lost to turning, which had been 8% of engine hours for the 300 m pass.  We decided to test a 600 m pass. But while it reduced the proportion of time spent turning to 4%, overall productivity barely nudged to 8.3 ha/h.  That’s a 4% improvement, not worth removing any trees over.

    One of the biggest game-changers in sprayer productivity has been the 3” transfer pump and efficient product induction systems. Reducing fill time from 30 to 15 minutes did have a large effect here too, increasing productivity to 9.3 ha/h, a 16% increase from the base. There remain inefficiencies in the system, such as the time spent with partial jugs that require measuring. A faster pump doesn’t address these. But perhaps a closed transfer system can.

    With the travel time associated with a home fill being such a large time consumer, introducing a field-based tendering system was expected to have a large impact. We combined this with a fast fill because a proper tender unit would have the larger pump. And the results were impressive, a jump to 13.7 ha/h. That’s a 72% increase from the base scenarios, boosting spray efficiency to 38%. 

    The final scenario involves two large changes. A new, larger sprayer with a 5000 L tank and 36 m boom, combined with a fast fill tendering system. And the results were equally large, boosting productivity to 19.8 ha/h, more than doubling the performance of the base condition (a 148% improvement). Spraying efficiency did not increase further from the fast-filling tendering system alone, because the faster filling was accompanied by the faster emptying of the wider boom.

    What is the value of this study? For one thing, we learned that a change that works in one geographic area may not work in another. For these smaller field scenarios, the benefit of a wider boom was undermined by the long downtime during fills. And obtaining a tender system when a single sprayer fill can cover a whole field wasn’t a slam dunk like it is elsewhere, where a field often requires several fills.

    Does a producer actually need to spray everything faster? The answer will depend on each farm. A general observation we’ve made is that the windows of opportunity for spraying are getting narrower. Restrictions on wind speed or temperature leave fewer hours in a day to get the spraying done. The risk of falling behind is lurking. And that means that application may not get done when they’re most effective. Disease may have progressed. Weeds will have grown. Crop safety may be challenged. Being even a little more productive can help mitigate all those risks.

    If nothing else, it’s critical for an applicator to know where the time goes. Use the calculator. Only then can you be strategic about correcting a problem. 

  • We Need Better Drift Control Technologies

    We Need Better Drift Control Technologies

    Sprayer manufacturers have all but offloaded the entire responsibility for drift management to the sprayer nozzle. It’s asking too much.

    Sprayers have changed a lot over the past 25 years. They have become larger, with more tank capacity, boom width, and, if self-propelled, horsepower.  They are more comfortable and ergonomic, with more sophisticated swath control and guidance systems. But every year, a very important deficiency in their design becomes obvious. Drift control.

    The changes described above are intended to improve productivity and fight operator fatigue.  Today’s sprayer can cover more ground than ever before. But the demand to cover ground, through a combination of growth in farm size and frequency of treatment, has outpaced machine productivity. As a result, operators find themselves ever further in a time deficit, with acres on the to do list and no time to get the work done.

    Spray drift remains the single most limiting factor to the safe application of pesticides. Spraying cannot happen when it’s too windy or during inversions because all agricultural nozzles produce fine droplets whose movement in the atmosphere cannot be controlled. This has been an issue since spraying began.

    Simply put, pesticides belong in one place only, and that is on the treated swath.  Applicators have some tools to make this happen, such as using coarser sprays, lowering the booms, choosing very specific weather conditions, and the like. But when winds are incessant, and crops and pests are quickly growing out of the treatable stages, what is an applicator to do?  There is only one thing they can do: lower their standards. Either miss the treatment and suffer the yield loss, or spray in the wind and hope nothing bad happens.

    Neither of these options are acceptable.

    There isn’t an easy fix. Spraying is a game of tight margins. The spray liquid in the tank must be atomized into droplets that can make their way to the target and provide adequate coverage when they get there. The total liquid volume to achieve that task must also be practical. The global ag industry has determined, over the past 100 years, that about 100 to 200 L/ha, 10 to 20 gallons per acre, is the ballpark amount that allows reasonable work rates with sprays that are just coarse enough to resist displacement in modest winds.  If it gets windier and we need even coarser sprays, we need to add more water to maintain an acceptable droplet density on the targets. And of course, the droplets need to stick to those targets, so there is a limit how coarse we can spray.

    Over the past 20 years, we’ve been asking the low-drift nozzle to do the heavy lifting in drift management, and it has served us well. But with a return to more contact modes of action for resistance management, there’s a need to retain good coverage for product performance.

    What ag needs is a drift-reducing technology that is better than the low-drift nozzle. We need a technology that maintains a practical water volume limit and combines this with intermediate spray qualities that generate good pesticide efficacy without allowing drift under windy conditions.

    These technologies need to do just one of three things: (a) Protect the driftable droplets from exposure to moving air with a physical barrier, (b) make driftable droplets less drift-prone by increasing their velocity, or (c) eliminate the driftable droplets altogether.

    Let’s have a look at some options, and explore the pros and cons.

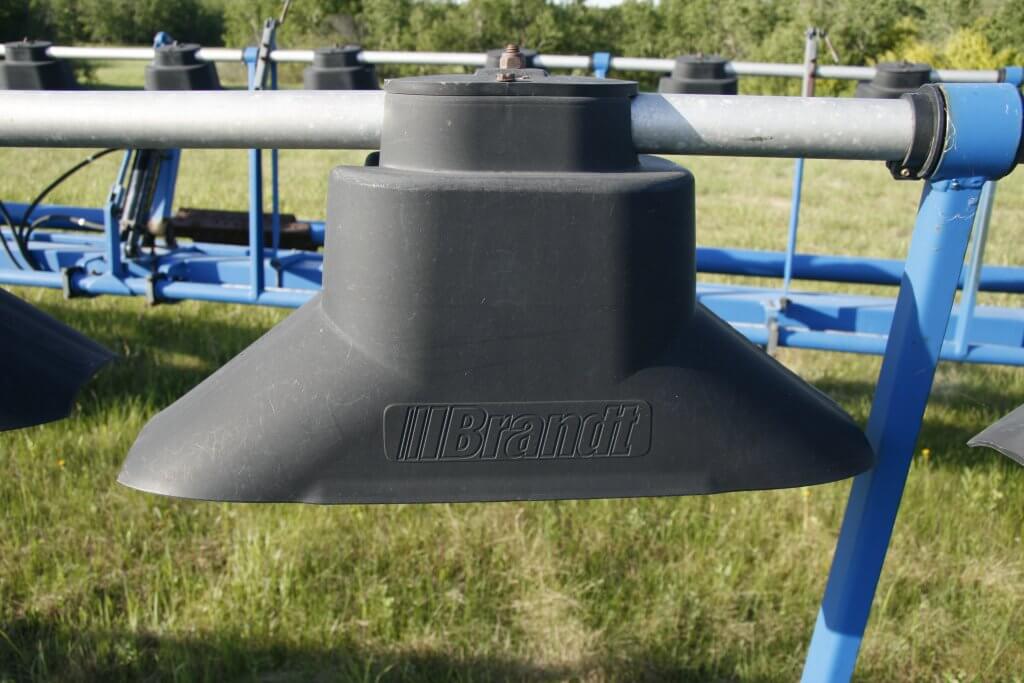
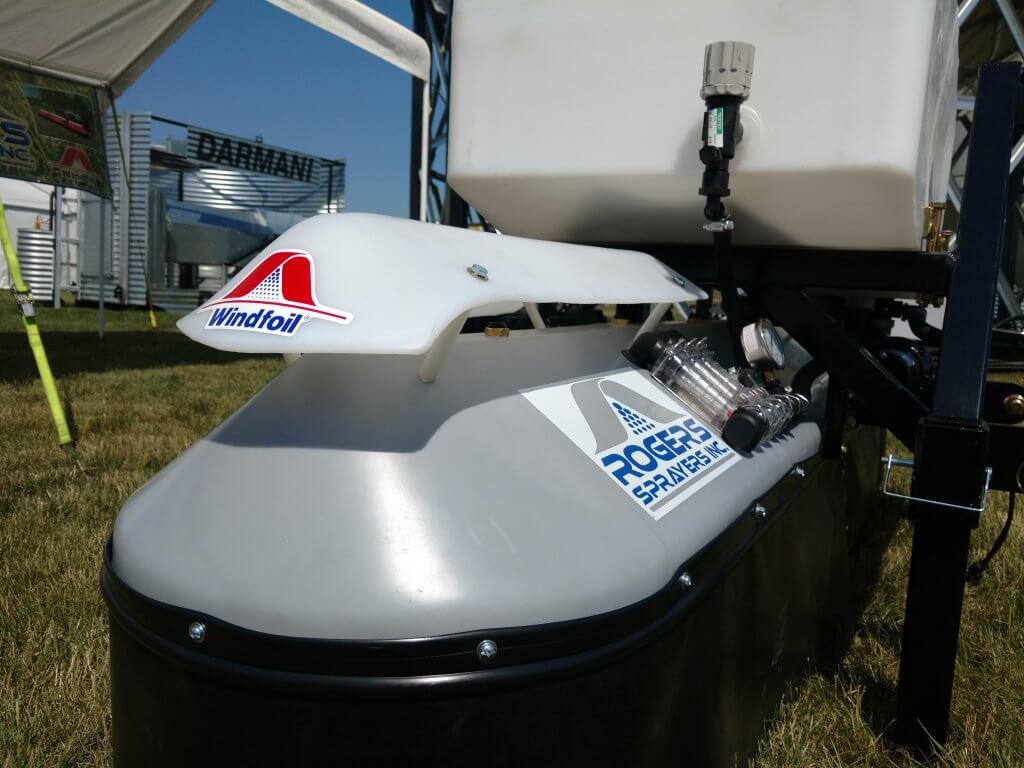
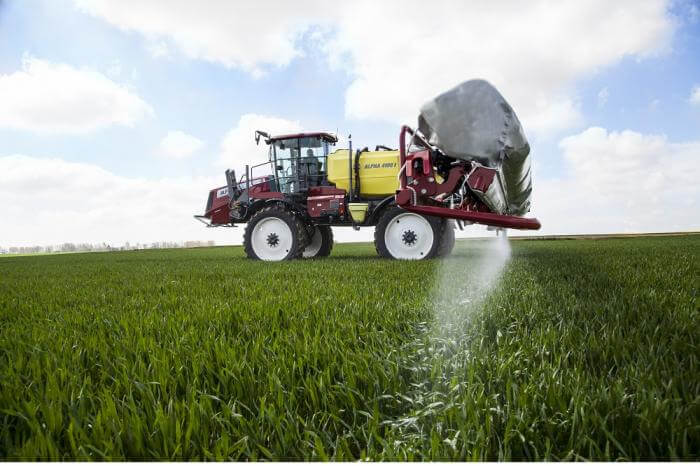
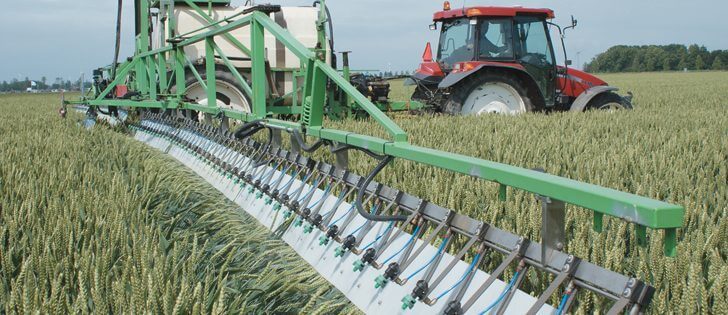
    Shields and Cones.  A shroud surrounding the boom was first proposed and built in the 1950s in the UK by Dr. Walter Ripper. Although never commercial, his “Nodrif” boom inspired an entire industry that took hold in western Canada in the 1980s and 1990s. Shrouding worked. In studies conducted at Ag Canada, shrouds produced by Flexi-Coil, Rogers Engineering, AgShield, and Brandt reduced drift by up to 80%. But shrouds disappeared in the 90s, partly because of the advent of tight-folding suspended booms where their physical size posed a problem, but also because of crop contamination from the shrouds and poor nozzle visibility in case of blockages.

    The advent of the air-induced low-drift nozzle offered an alternative, but coarseness has been taken to its practical limit. 

    What about a newly engineered version of shrouds that addresses its shortcomings? Willmar Fabrication has created the Redball Buffer Sprayer, for example. We see hooded sprayers in row crops. But there may be other ideas. The simple device called the PatternMaster introduced by KB Industries a few years back was also a step in that direction. Let’s keep working on this.

    Figure 1: Shrouded booms, once common on the prairies and proven effective (Brandt cones, top), are still used on research and turf sprayers (bottom).

    Air Assist. Small drops don’t drift just because they’re small. They drift because they have very little kinetic energy, and they get blown off course easily. Speed them up, and that problem is solved. Introducing an air stream at the nozzle can do just that. Furthermore, air assist also enhances canopy penetration, a problem that we currently attempt to address with the addition of more water. Again, this idea is not new. Hardi, once the world’s largest sprayer manufacturer, has had the TwinForce boom available for decades. An inflatable bag is positioned over the boom. Openings along the bottom direct the air down. The operator turns a knob in the cab to control fan speed, and another for forward or backward angle, until the combination is suited to the canopy and the travel speed. The SprayAir, out of Carseland, AB (purchased by Miller but no longer available) was a less elegant version because they chose an air-shear atomizer that sometimes required more air than was prudent. Too much air rebounds off the ground, increasing the drift issue. Their Trident boom, allowing a hydraulic nozzle to be used with air assist, continues to have potential.

    Air bag type air assist systems were also available from other manufacturers, but none were ever commercially successful.

    Figure 2: Air assisted booms such as this Hardi TwinForce accelerate small droplets, reducing their drift-potential and improving canopy penetration (Source: Hardi Sprayers)

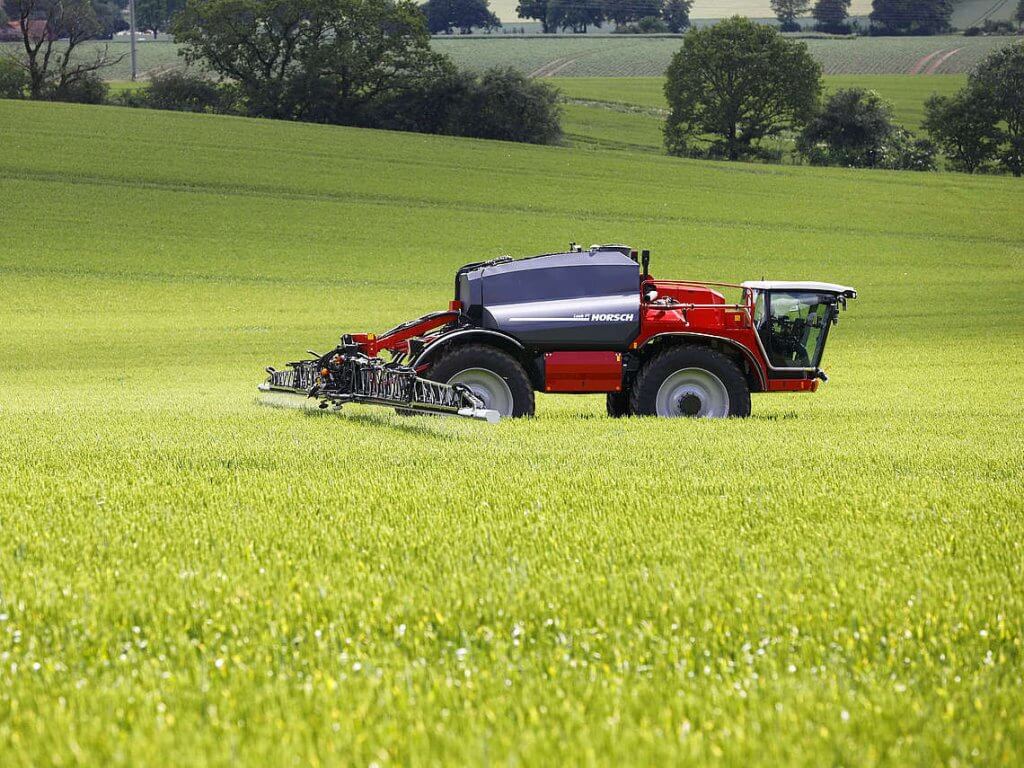
    Low Booms.  How low can booms go? It depends on the nozzle spacing and fan angle. Horsch claims that with a good boom package, this is an option. They are offering 10” spacing, and with wide fan angles, booms as low as 15” would still provide good overlap. Hands up who will try this at 18 mph. Wingssprayer has an interesting design where the boom rests on backswept plastic sheets, providing a physical barrier and a low height.

    Figure 3: Low booms can significantly reduce drift, but their success depends on superior stability and height control (Top, Source: Horsch Sprayers; Bottom, Source: Wingssprayer)

    Twin Fluid Atomizer. In this atomizer type, both air and liquid are forced out through the same nozzle. The ratio of air and liquid determines the liquid flow rate and the degree of atomization. First introduced by Cleanacres in the UK as the Airtec, improved by Harry Combellack in Australia over many years, and making a re-appearance with the Dutch manufacturer Agrifac, it’s been one of my favourite atomizers.  The small amount of air moving through each nozzle is not enough for serious air-assist, but the idea is good and perhaps it can be improved.

    Figure 4: A twin fluid atomizer utilizes air (entering from hose) and liquid (entering from boom) to create a spray whose droplet size and flow rate are adjustable. Air generates some assist to reduce drift.

    Electrostatics. Forget about it for drift control. The attractive force is so weak that it only works for very small droplets over short distances. It needs air-assist to work properly. See point #2.

    Rotary Atomizer. These are common on aircraft these days, as rotary cages, offering a more consistent droplet size range that eliminates the largest, water-wasting droplets, and curtails many of the smallest droplets produced by hydraulic atomizers. These attributes are powerful and address the fundamental problem: If the small droplets drift, then let’s not produce them. In reality, rotary atomizers are used mainly to produce smaller droplets to save water in the aerial business, not really solving the drift problem. In the 1970s and 80s, the concept was advanced by Micron Corporation, led by Ed Bals and later by his son Tom. Although very successful in forestry and hand-held applications in arid regions where water posed a serious limitation, the transition to boom spraying never happened.

    Rotary atomizers are now making a comeback with drone sprayers. Though promising, the flow rate capabilities of spinning disks are lower than those of the cages mounted on crewed aircraft. As a result, the disk may flood, and will no longer produce the desired monodisperse distributions.

    Figure 5: Rotary atomizers can eliminate larger droplets and sharply reduced the smallest ones, leaving a more uniform sized distribution (insert). They are used on aircraft to save water, but have not been adopted on ground equipment to control drift.

    A new Atomizer. All hydraulic nozzles produce a wide variety of droplet sizes, and that variety has provided robust performance over a wide range of conditions. But it can also be a problem. Even the venerable dicamba nozzles that create Extremely Coarse and Ultra Coarse sprays produce some fines that drift in inversions. The idea put forth by Ed Bals, to eliminate the problematic size ranges, is sound. But the rotary atomizer is hard to implement on a boom sprayer. Can there be an innovation that maintains a simple overall design, produces a narrow, but low-drift droplet size range, and mates it to a bit of air assist to get the spray where it belongs? Absolutely.

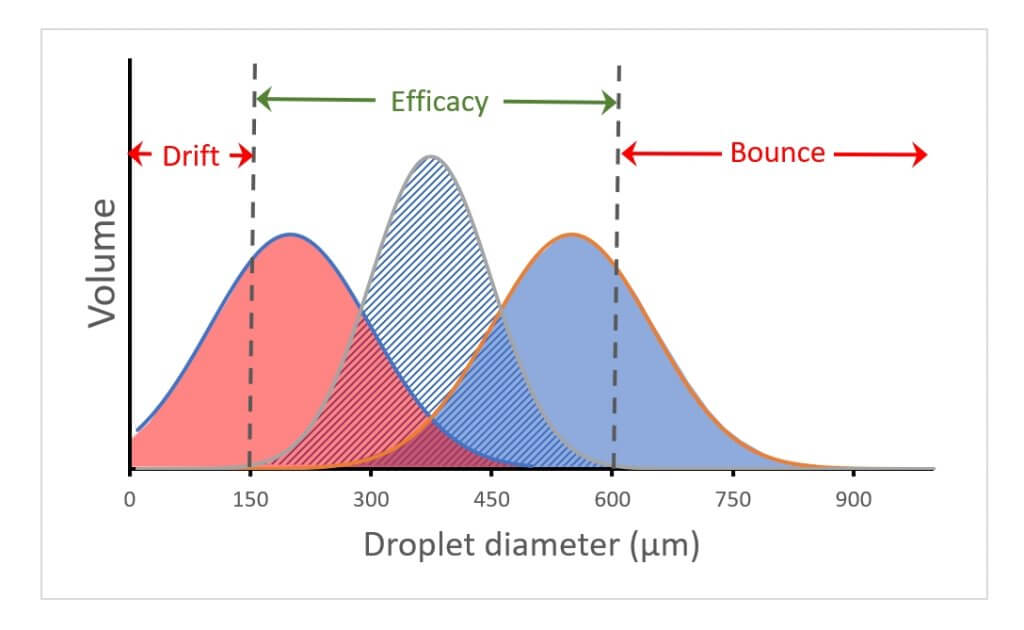
    Figure 6: Current hydraulic atomizers tend to produce a wide range of droplet sizes. The distribution on the left results in significant drift (droplets <150 µm). The one on the right wastes the larger droplets (droplets >600 µm. The narrower span in the centre distribution avoids these problem areas and delivers the spray in an efficacious portion.

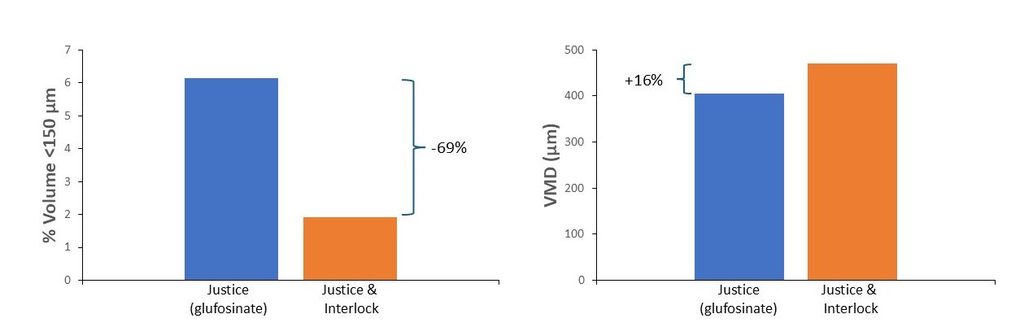
    Adjuvants. One of the problems with low-drift nozzles is their tendency to generate some very large droplets. These droplets are not very abundant and therefore don’t contribute to coverage, but they nonetheless consume significant carrier volume. The current generation of oil-based drift-reducing adjuvants (DRAs) have helped reduce the drift-prone size fraction without increasing the largest droplet size fraction as much as low-drift nozzles do. This more surgical approach is welcome. Unfortunately, the drift-reducing effect is not as much as low-drift nozzles alone can achieve. A combination of these two technologies is likely the best way forward.

    Figure 7: Effect of DRA on driftable fines (left) and overall volume median diameter (VMD, right) from AIXR11004 tip. Data courtesy Winfield United.

    Targetted Sprays. An obvious way to reduce drift is to spray less. With recent developments in camera-driven spot spraying, this is already happening. It’s safe to assume that every percentage not sprayed is an equivalent reduction in drift potential. And with reports of 50 to 90% savings, this will be significant. How these product savings are deployed remains important. Some applicators choose to raise pesticide rates to effect better control, and this of course negates some of the gains. Others are increasing the overall spray volume. This then opens the door to the use of coarser sprays without loss of coverage, enhancing gains.

    Figure 8: Spot spraying (Courtesy Croplands)

    To create value for farmers you first need to understand farmers’ priorities and problems. Getting the spraying job completed on time often means squeezing the work into ever narrower time frame, between rains, between winds in the afternoons and inversions that same evening, between too much dew and too dry, between too early and too late. I am looking forward to the day when engineering resources are allocated to address these issues better, protecting both the environment and the stress levels on the farm.

  • Increase Sprayer Productivity Without Driving Faster

    Increase Sprayer Productivity Without Driving Faster

    Timing trumps most things in crop protection. A great spray applied at the wrong time isn’t nearly as valuable as a mediocre spray at the right time. So how do we improve our ability to get things done at the right time?

    Often, we try to win races by driving faster. In our last article, we looked at driving speed and concluded that faster speeds can lead to more drift and less uniform deposition. Driving slower can be viewed as a sort of insurance policy: You may not notice the benefits right away, but on days when that extra bit of performance is required, you’re covered.

    So how do you get the job done quickly if you can’t drive faster?  To answer, we have to look to other opportunities for boosting productivity.

    Recently, we used our and tried to capture all the elements of a normal spray operation that affect timeliness. These were:

    • travel speed
    • boom width
    • tank size
    • water volume
    • field length
    • number of headlands
    • turning speed
    • fill time

    First, we identified a reasonable base condition. For the sprayer, that was a travel speed of 14 mph, a 90’ boom, an 800 gal tank, a 10 gpa water volume, and a 20 minute fill time. Then, we set up a typical field situation, which was spraying a half-mile run on a quarter with two sprayed headlands and a turning speed of 8 mph. Finally, we changed one factor at a time to determine its relative importance.

    Before we discuss the results, let’s make it clear that just because changing some of these factors improves productivity doesn’t mean we’re recommending them! For example, adequate water volume remains an important input that improves coverage and permits the use of low-drift sprays. Larger tanks increase compaction and take more power, and so forth.

    Here’s what we found:

    All productivity values were expressed as acres per engine hour. For this reason, our numbers will be lower than what a typical sprayer monitor reports, most of which calculate acres per spraying hour.

    For the base condition, the sprayer spent 15% of its driving time turning, and 37% of its on-field time stationary (i.e. filling or cleaning).  For every hour spent on the field, less than half the time (48%) was spent spraying. This resulted in an average productivity of 82 acres/h.

    Increasing the spray speed to 18 mph increased average productivity to 93 acres/h, but it also increased the proportion of time spent turning and loading, resulting in just 40% of the field time spent spraying.

    Decreasing the loading time from 20 to 10 minutes reduced the proportion of field time spent stationary to 23%, covering 100 acres/h at 14 mph. Surprisingly, this was the productivity-winner, resuling in 62% of on-field time spraying.

    We discovered other powerful productivity factors, and chief among them was boom width. A 33% increase in boom width from 90’ to 120’ gave a productivity boost to 94 acres/h, close to the same result as increasing the travel speed to 18 mph earlier. Similar side effects occurred: more time turning, and a greater proportion of time filling, as we saw with faster travel speeds.

    Boom width seems to have some room for growth.  Many smaller European counties use wider booms than we do in North America, for example.  With gps guidance and large fields, we have excellent conditions for their implementation.

    Two other factors that had similar effects to fill time were water volume and tank size. Less water and larger tanks increased productivity by decreasing the fill frequency, with effects similar in magnitude to speeding up the fill time. Decreasing the water volume from 10 to 5 gpa increased productivity to 100 acres/h by decreasing the proportion of time the sprayer was stopped from 37% to 23%. Increasing from an 800 to a 1,200 gallon tank increased productivity to 94 acres/h, again by decreasing the proportion of time spent filling to 28%.

    Taken together, a sprayer with a 120’ boom, a 1,200 gal tank, applying 10 gpa and filling in 10 min had an average productivity of 132 acres/h. And this was achieved without driving faster than 14 mph. If you can string two quarters together and drive a whole mile before turning, that number rises to 145 acres/h, a surprisingly large 13 acres/h gain.

    The perspective of minimizing downtime extends to other tasks, too:

    • Be more prepared for the job by reviewing the product label in advance, noting the correct mixing order.
    • Keep extra nozzles, clamps, and nozzle bodies in the cab.
    • Don’t clean plugged nozzles, replace them.
    • Use low-drift nozzles so a small increase in wind doesn’t shut you down.
    • Ensure all the products needed are on the tender truck (e.g. pesticide, adjuvant, tank cleaner, anti-foamer, etc.).
    • Consider switching to 3” plumbing (pump rates of 300 – 400 gpm are possible).
    • Make sure your inductor won’t be the limiting factor. For example, product pumps can be awfully slow when the product is cold. It might be worthwhile to explore a venturi system.

    Speeding up the fill process is a good idea, but be careful with certain products. Dry materials such as the sulfonyl ureas (e.g. Refine, Express SG, etc.) and some fungicides (e.g. Astound, etc.) require time to hydrate in water so they mix properly. Some operators pre-hydrate these in a smaller tank, while others get an extra tank to pre-mix whole loads and simply transfer them over.

    Also think about the time spent cleaning the sprayer. Thoroughness is important, but perhaps there are efficiencies to be gained there as well, like never letting a sprayer sit after spraying. We’ve written about continuous rinsing, for example, to improve cleaning speed and effectiveness.

    So, the quicker we can spray, while ensuring a quality job, the more effective our crop protection practices will be. We encourage you to use our to determine your best configuration.

    Got a productivity tips to share? Let us know! And remember: In spraying, the race is won in the pits.

    Factor

    Base

    Drive Faster

    Fill Faster

    Spray Wider

    Less Water

    Bigger Tank

    New Sprayer

    Travel Speed

    14 mph

    18 mph

    14 mph

    14 mph

    14 mph

    14 mph

    14 mph

    Fill time

    20 min

    20 min

    10 min

    20 min

    20 min

    20 min

    10 min

    Boom Width

    90 ft

    90 ft

    90 ft

    120 ft

    90 ft

    90 ft

    120 ft

    Water Volume

    10 gpa

    10 gpa

    10 gpa

    10 gpa

    5 gpa

    10 gpa

    10 gpa

    Tank Size

    800 gal

    800 gal

    800 gal

    800 gal

    800 gal

    1200 gal

    1200 gal

    Field Length

    0.5 mile

    0.5 mile

    0.5 mile

    0.5 mile

    0.5 mile

    0.5 mile

    0.5 mile


    Time Turning

    15%

    19%

    15%

    20%

    15%

    15%

    20%

    Time Loading

    37%

    42%

    23%

    42%

    23%

    28%

    19%

    Time Spraying

    48%

    39%

    62%

    38%

    62%

    57%

    61%

    Acres/h

    82

    93

    100

    94

    100

    94

    132

    To work with the productivity calculator, click here.